


Industrial Automation
Industrial Computers for Factory Automation
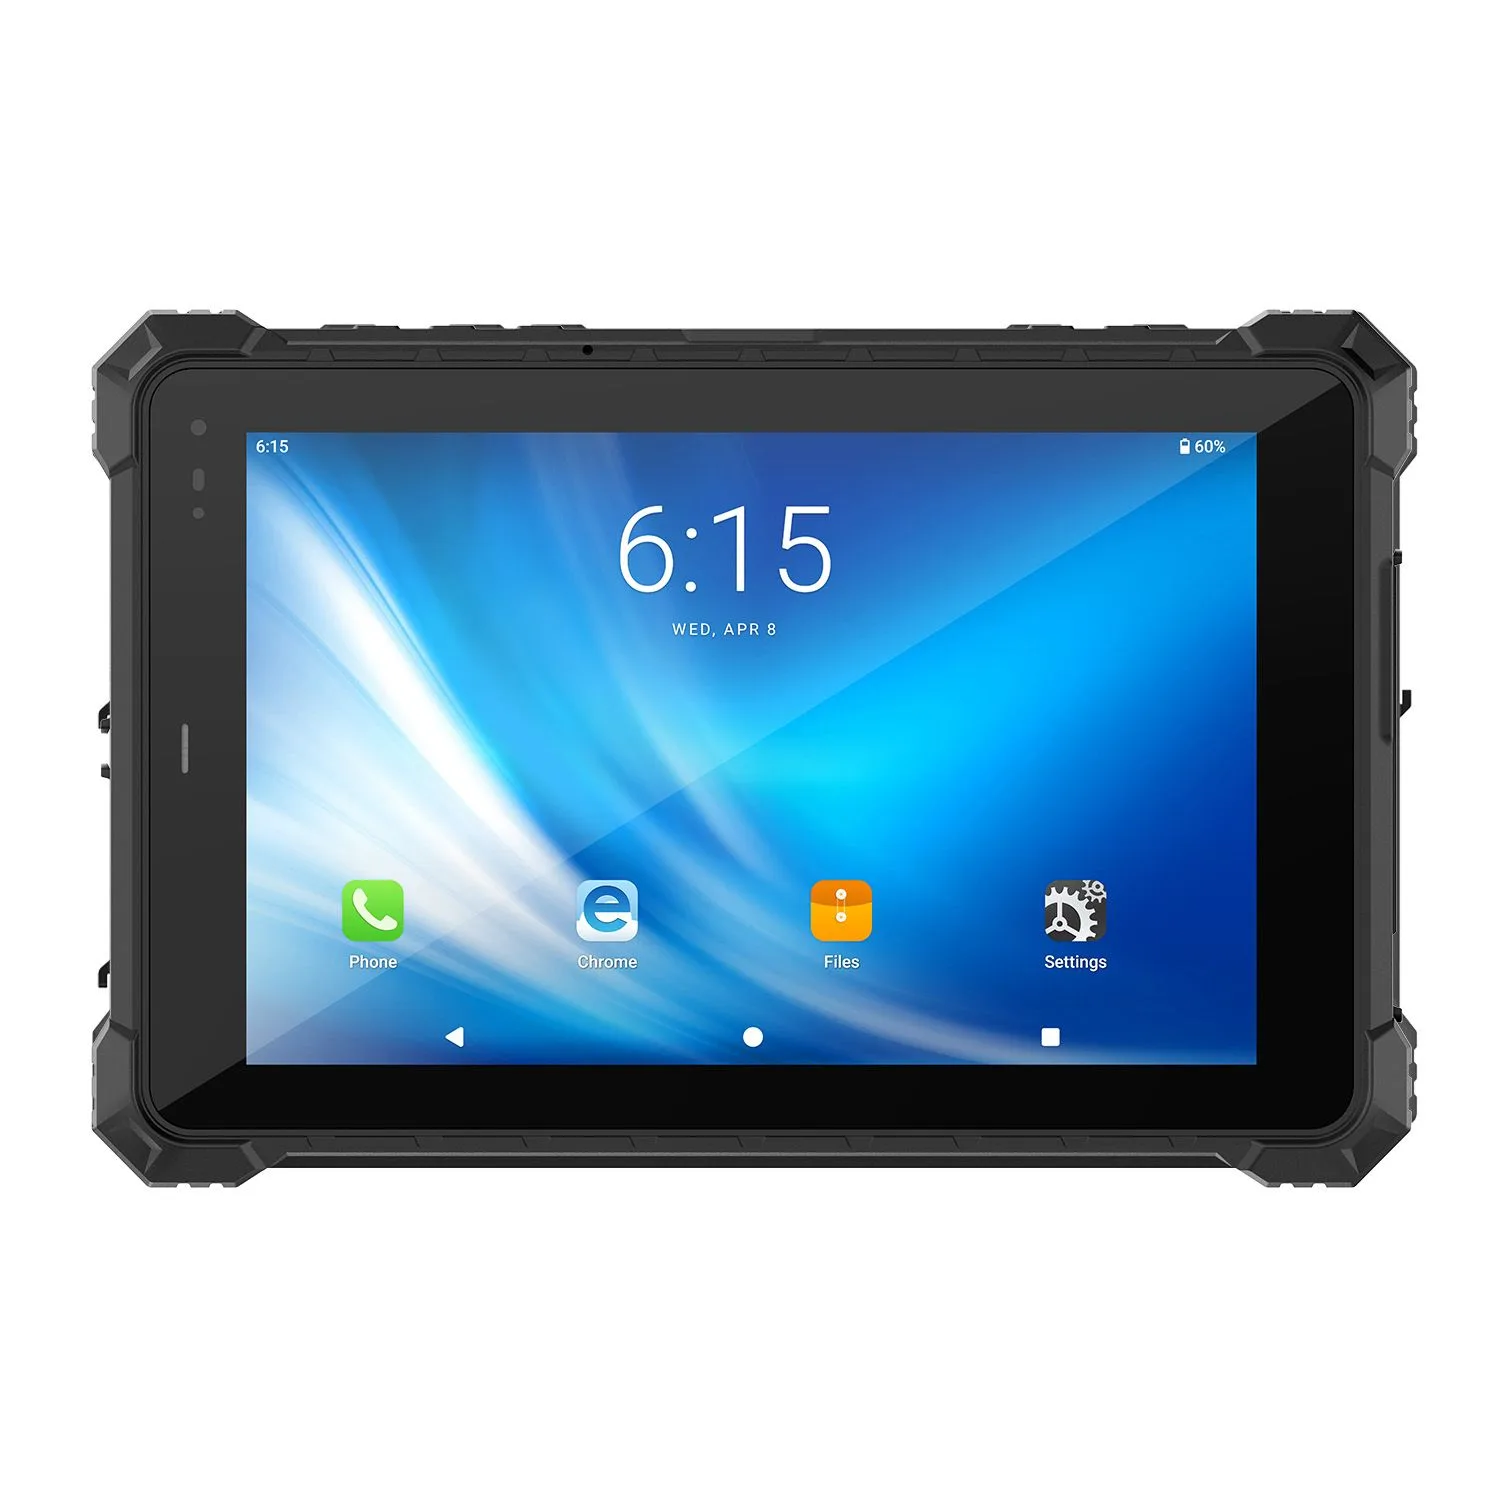
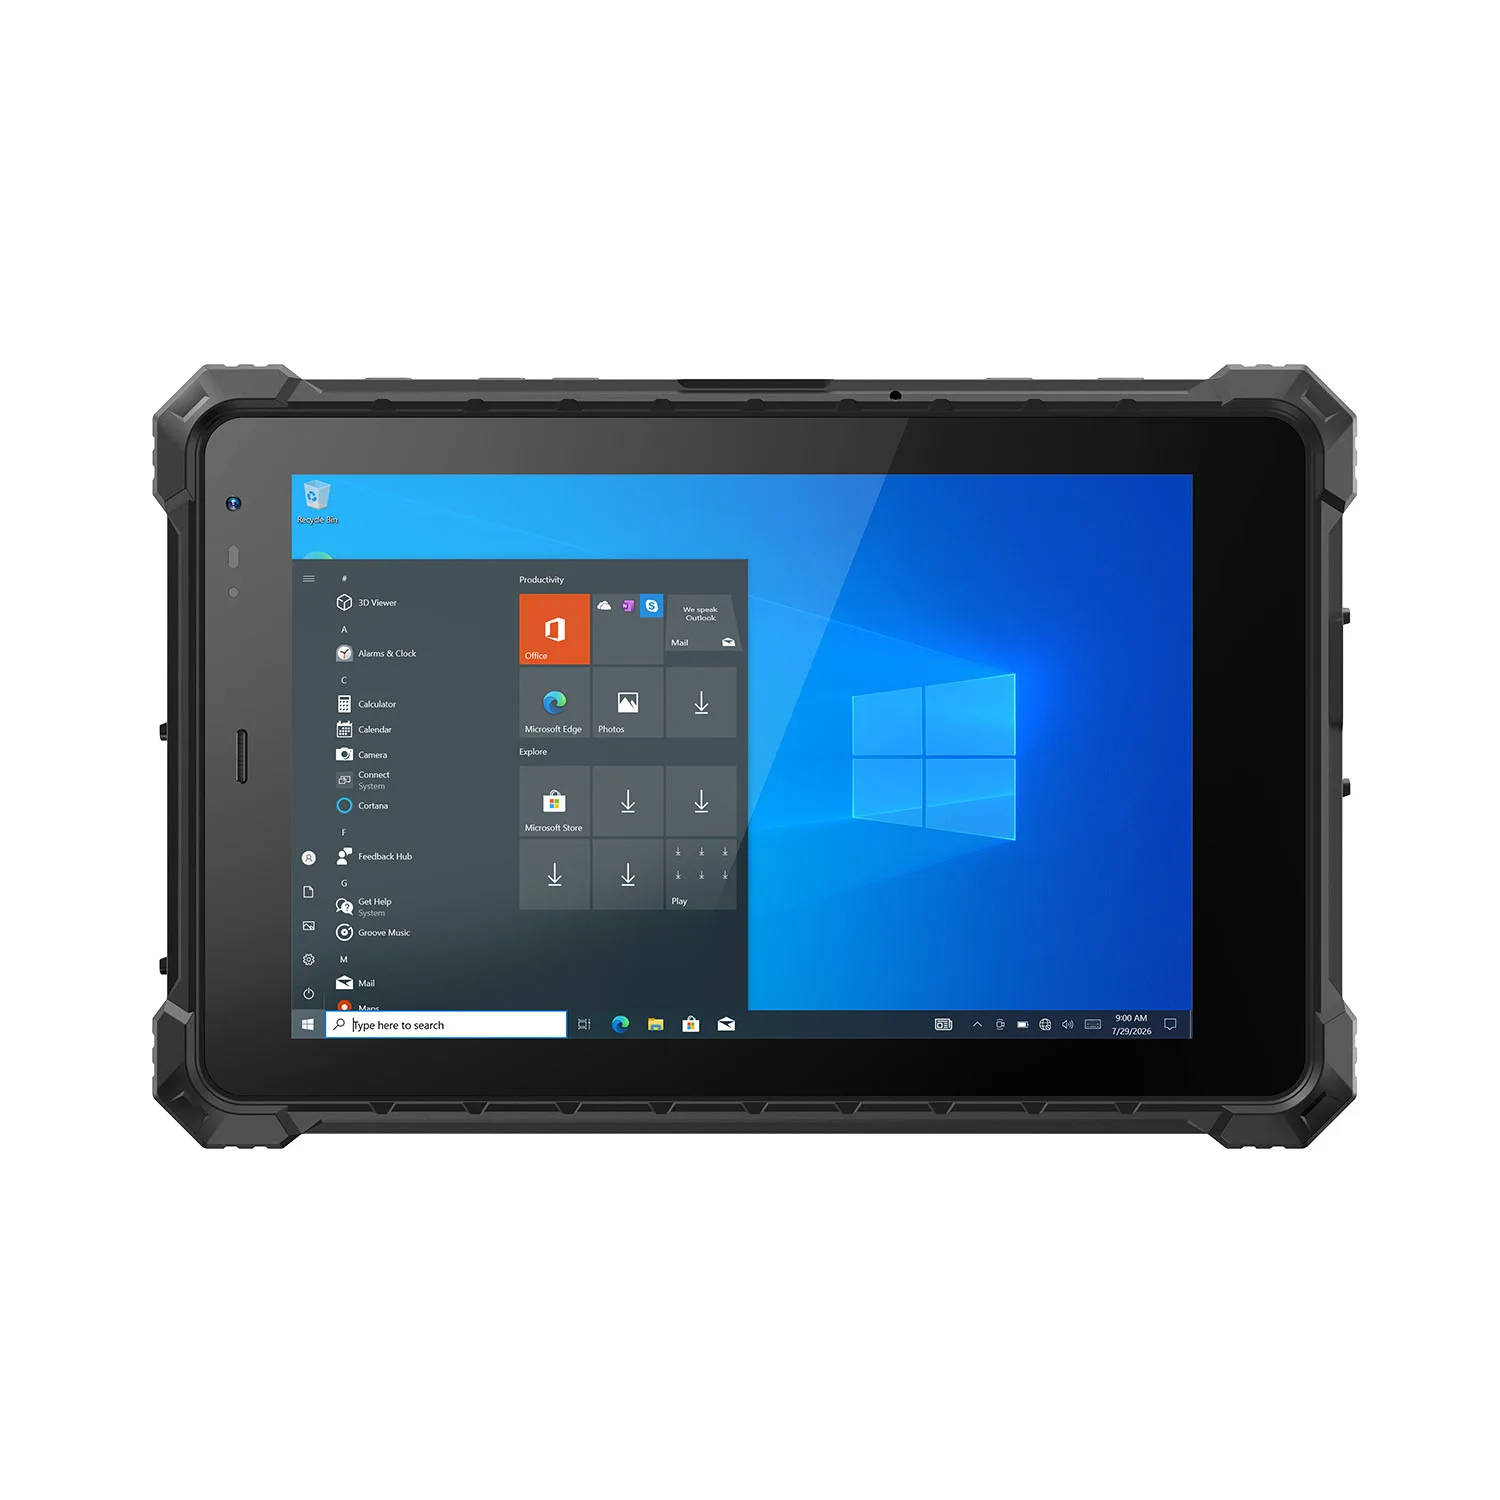
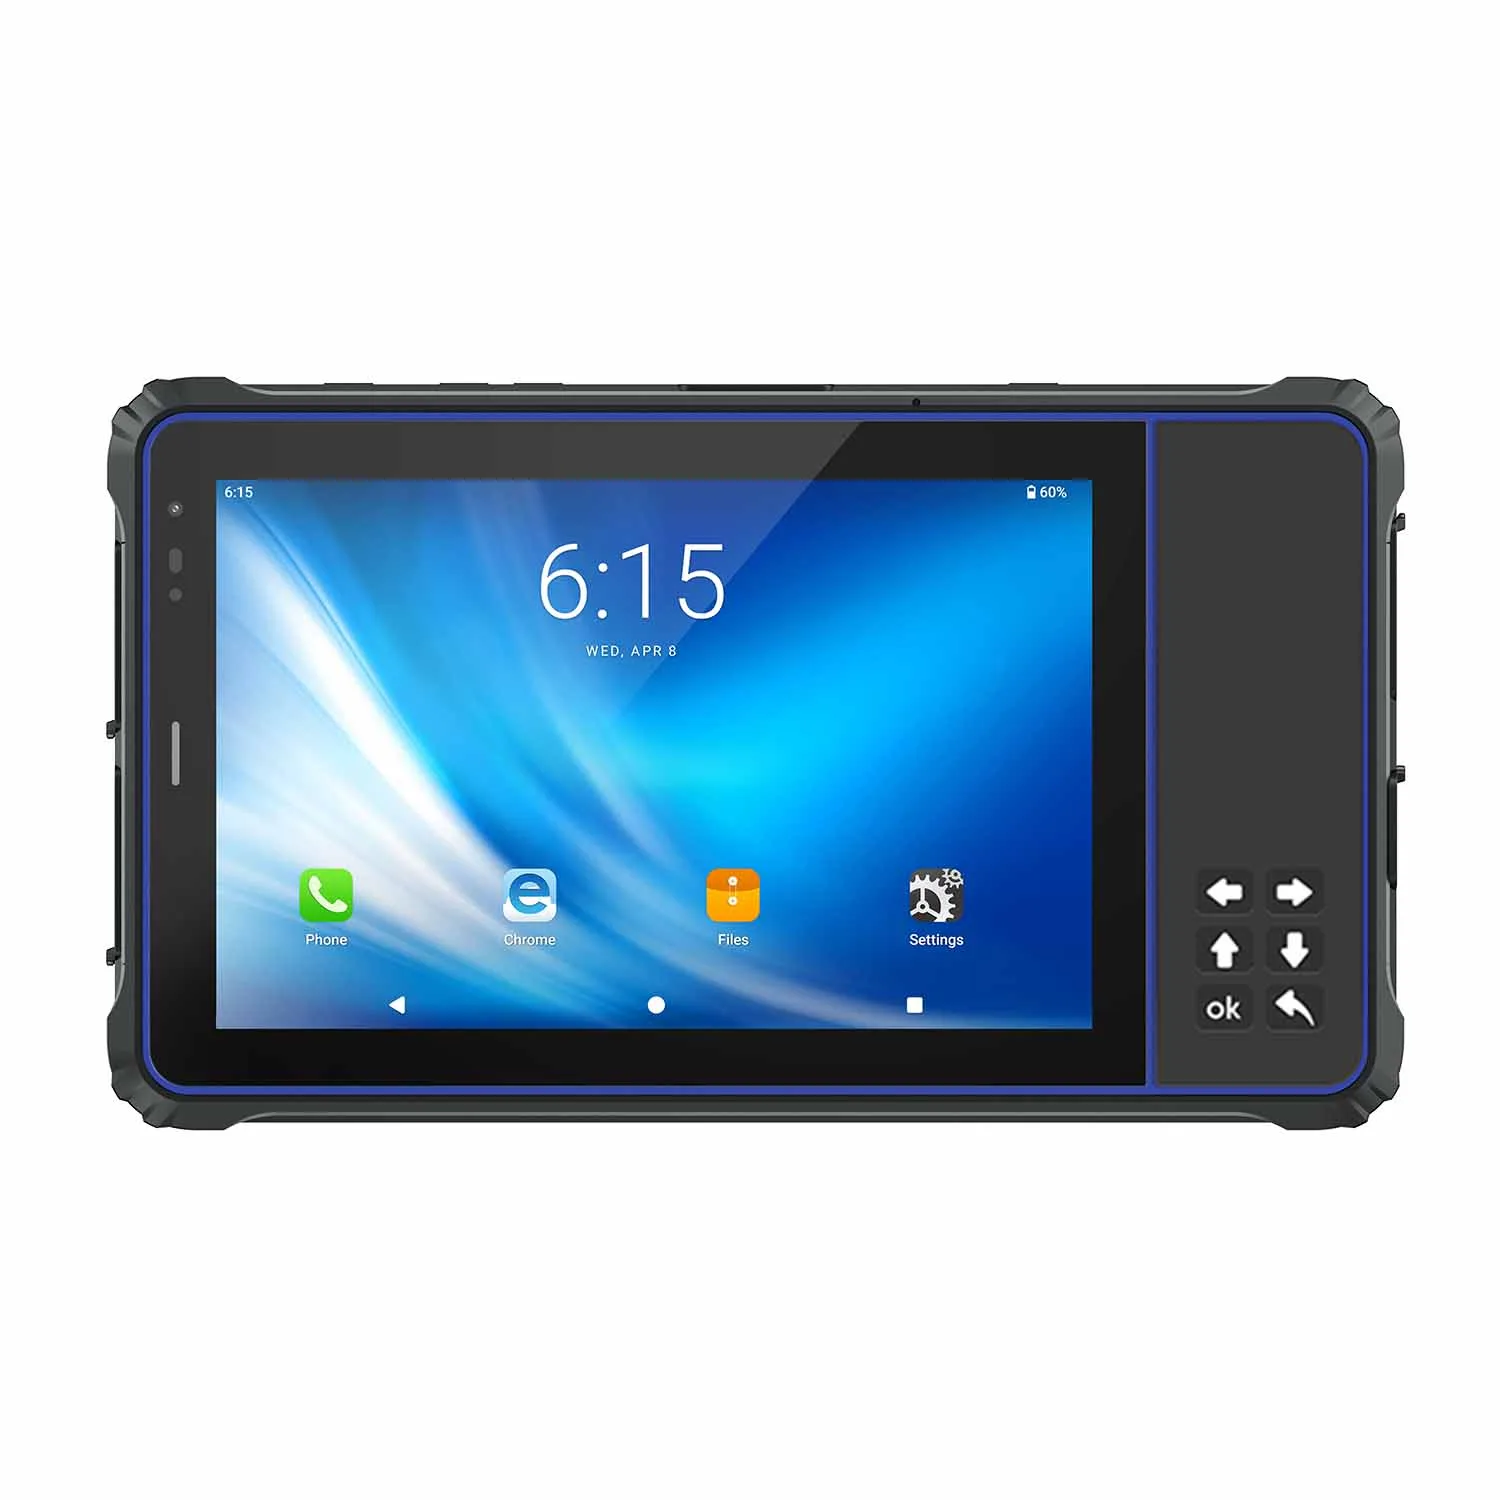
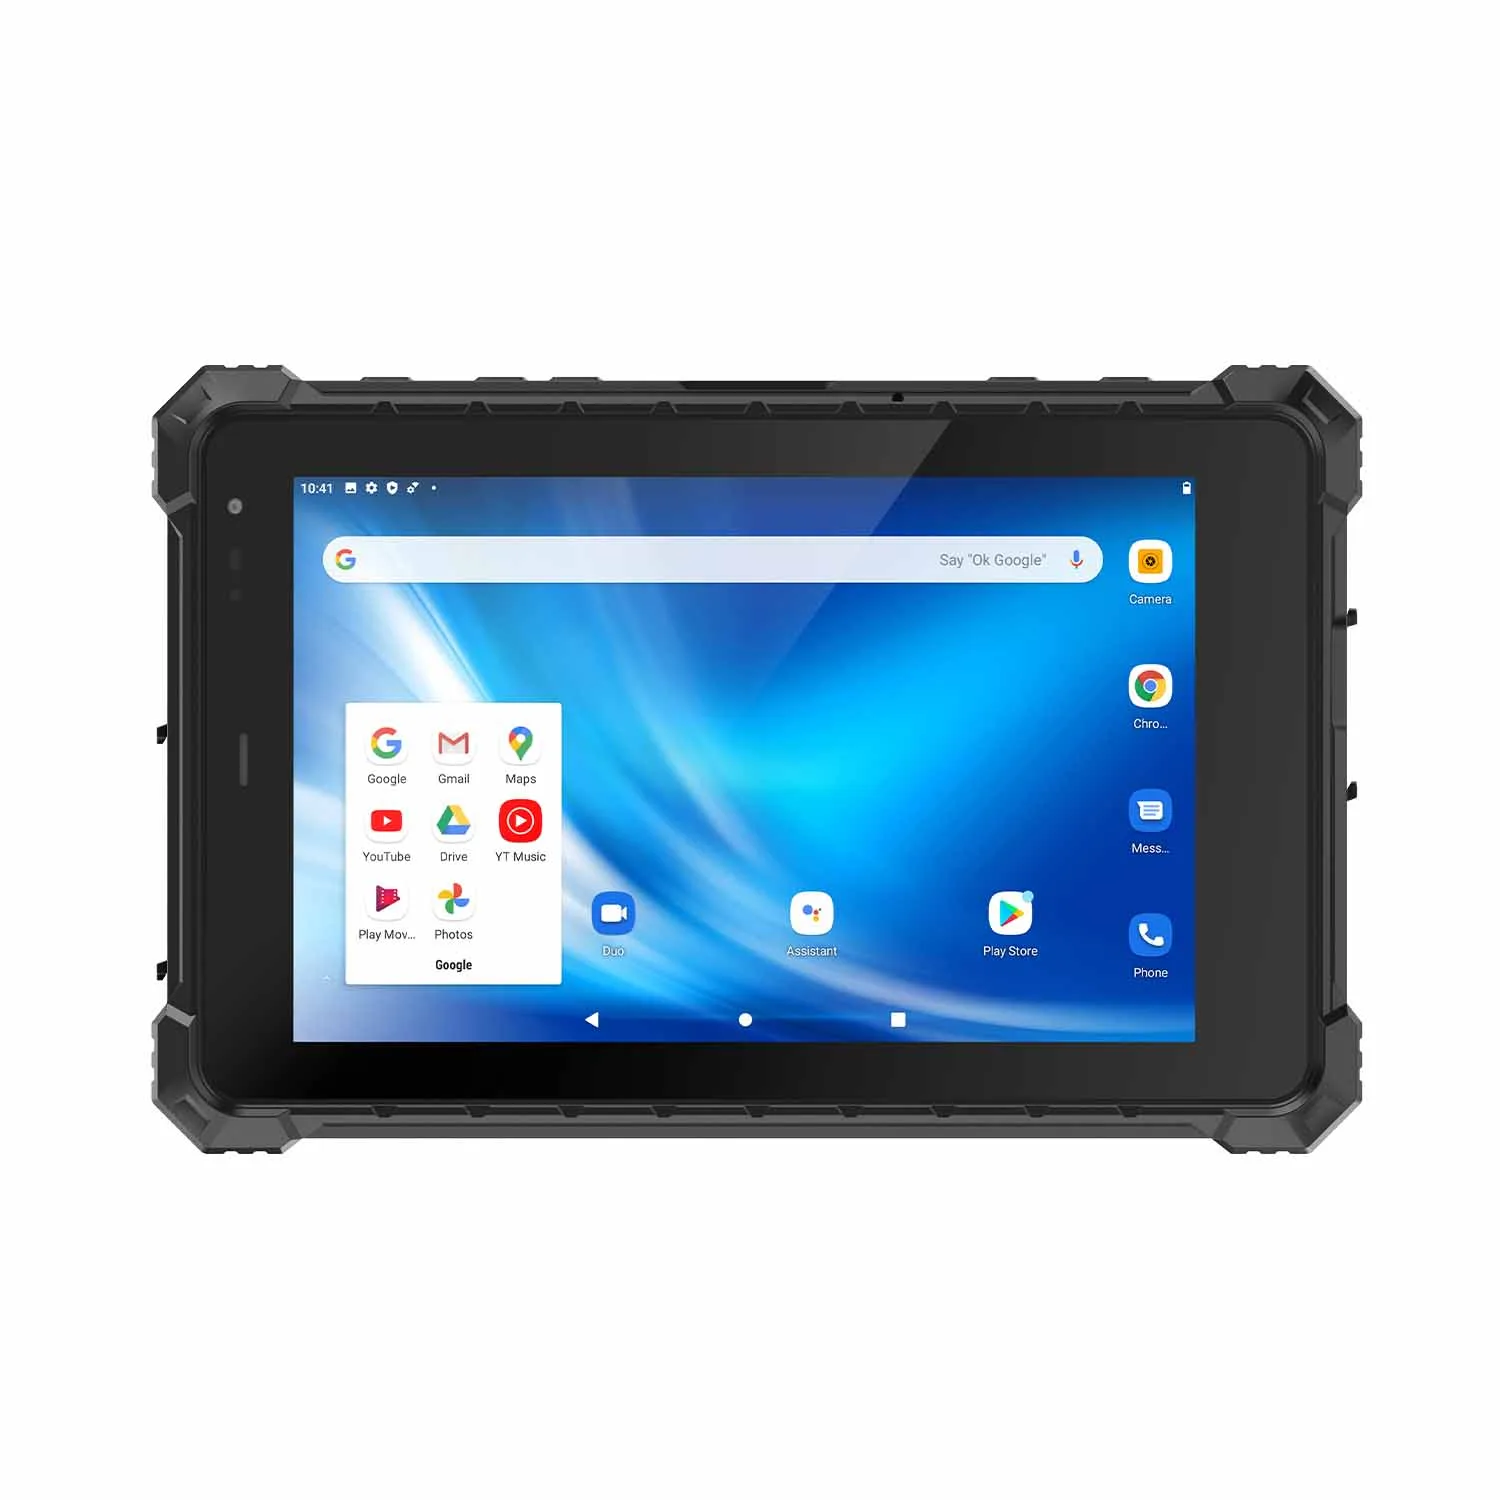
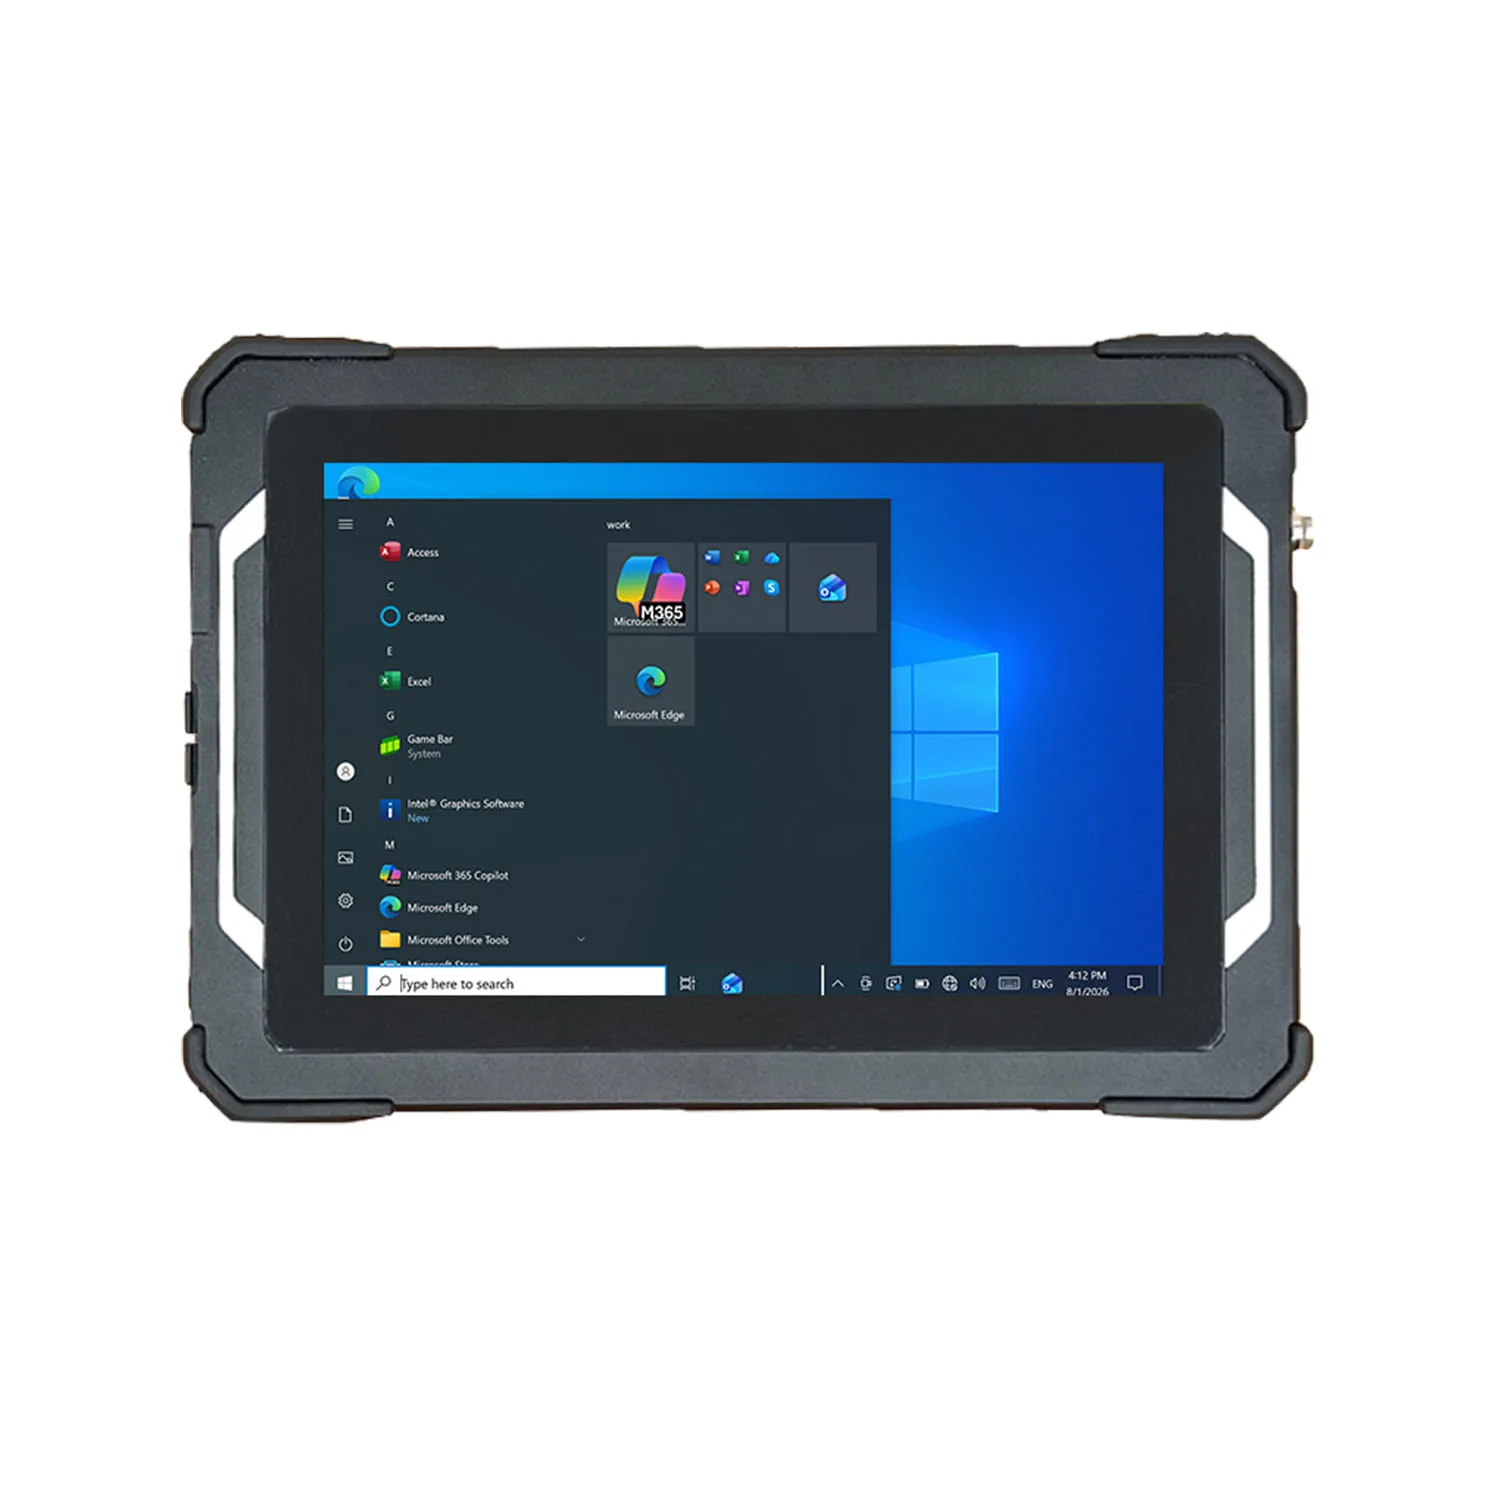
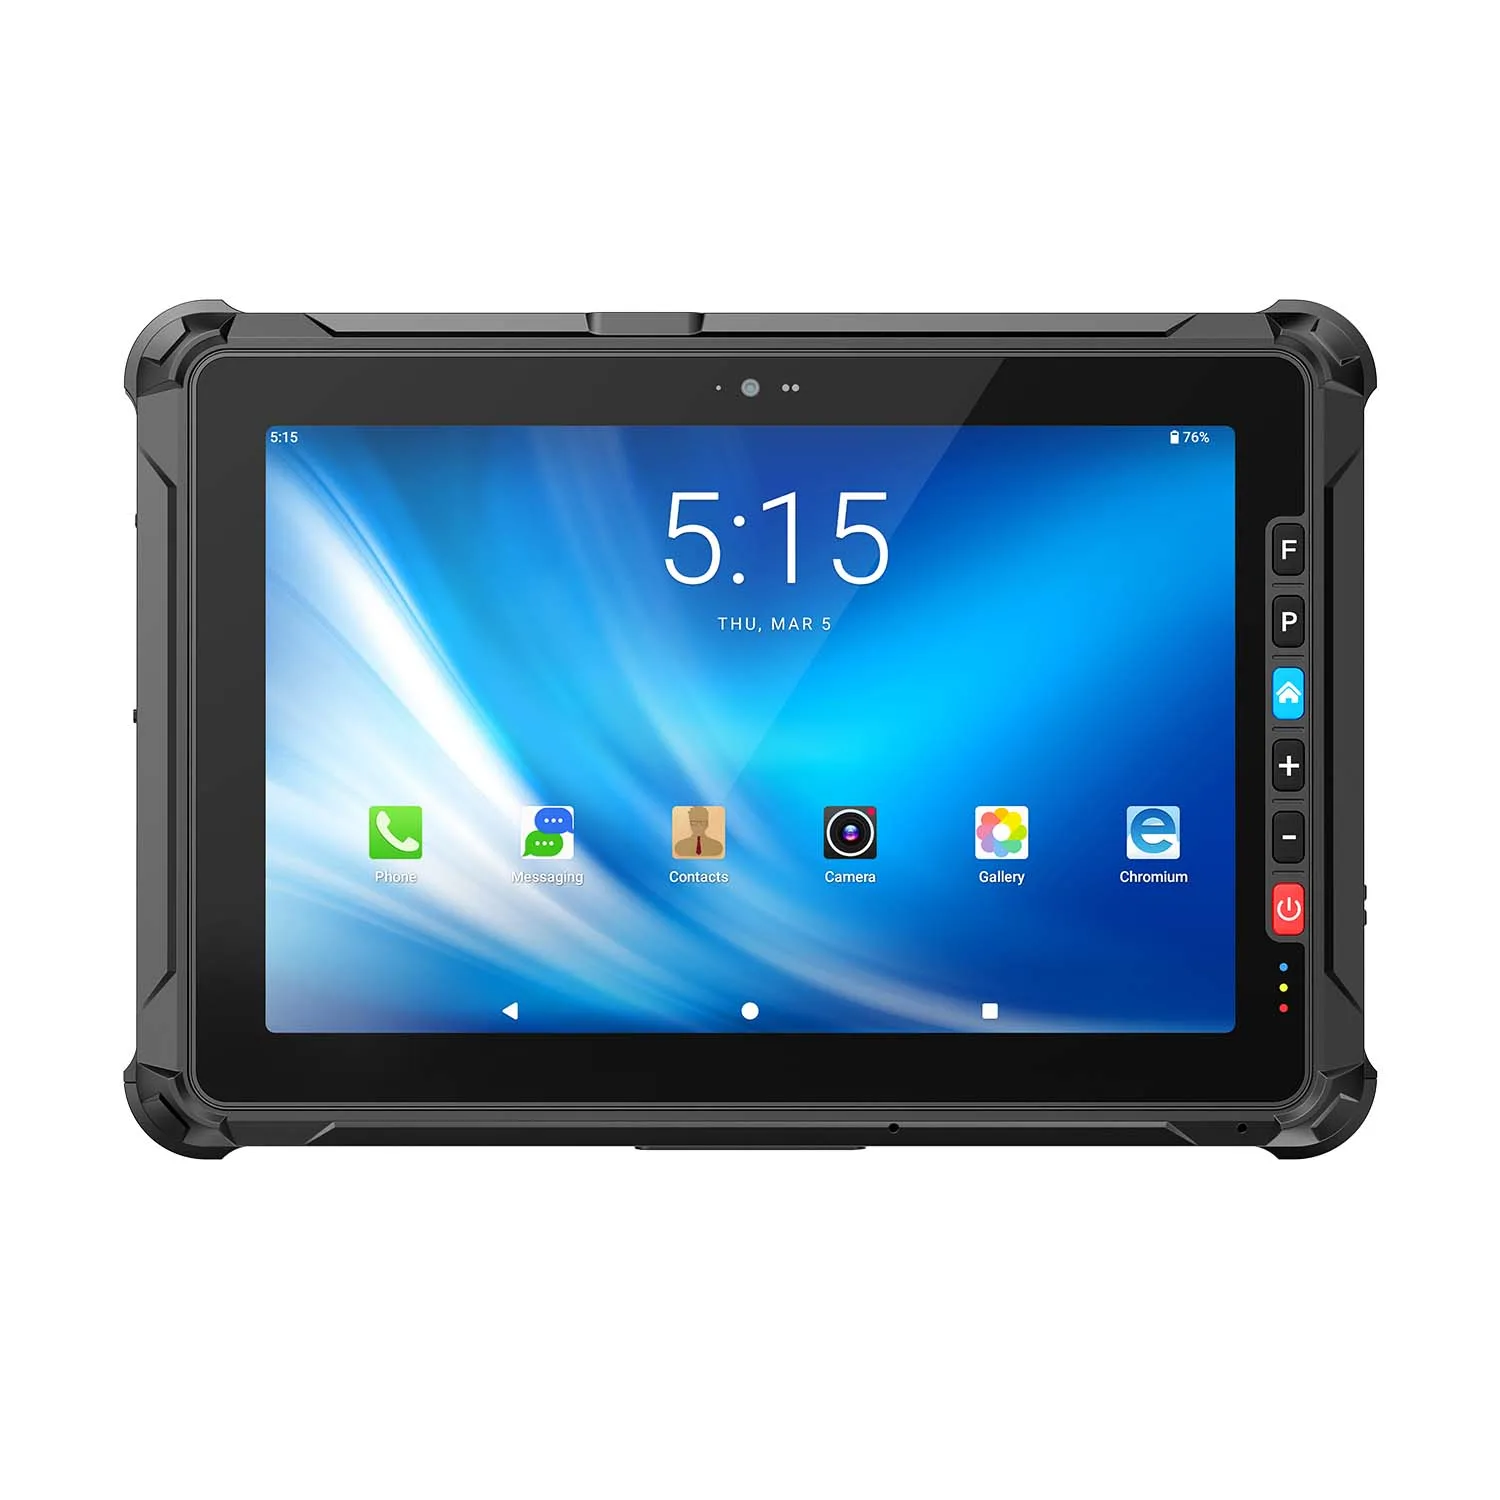
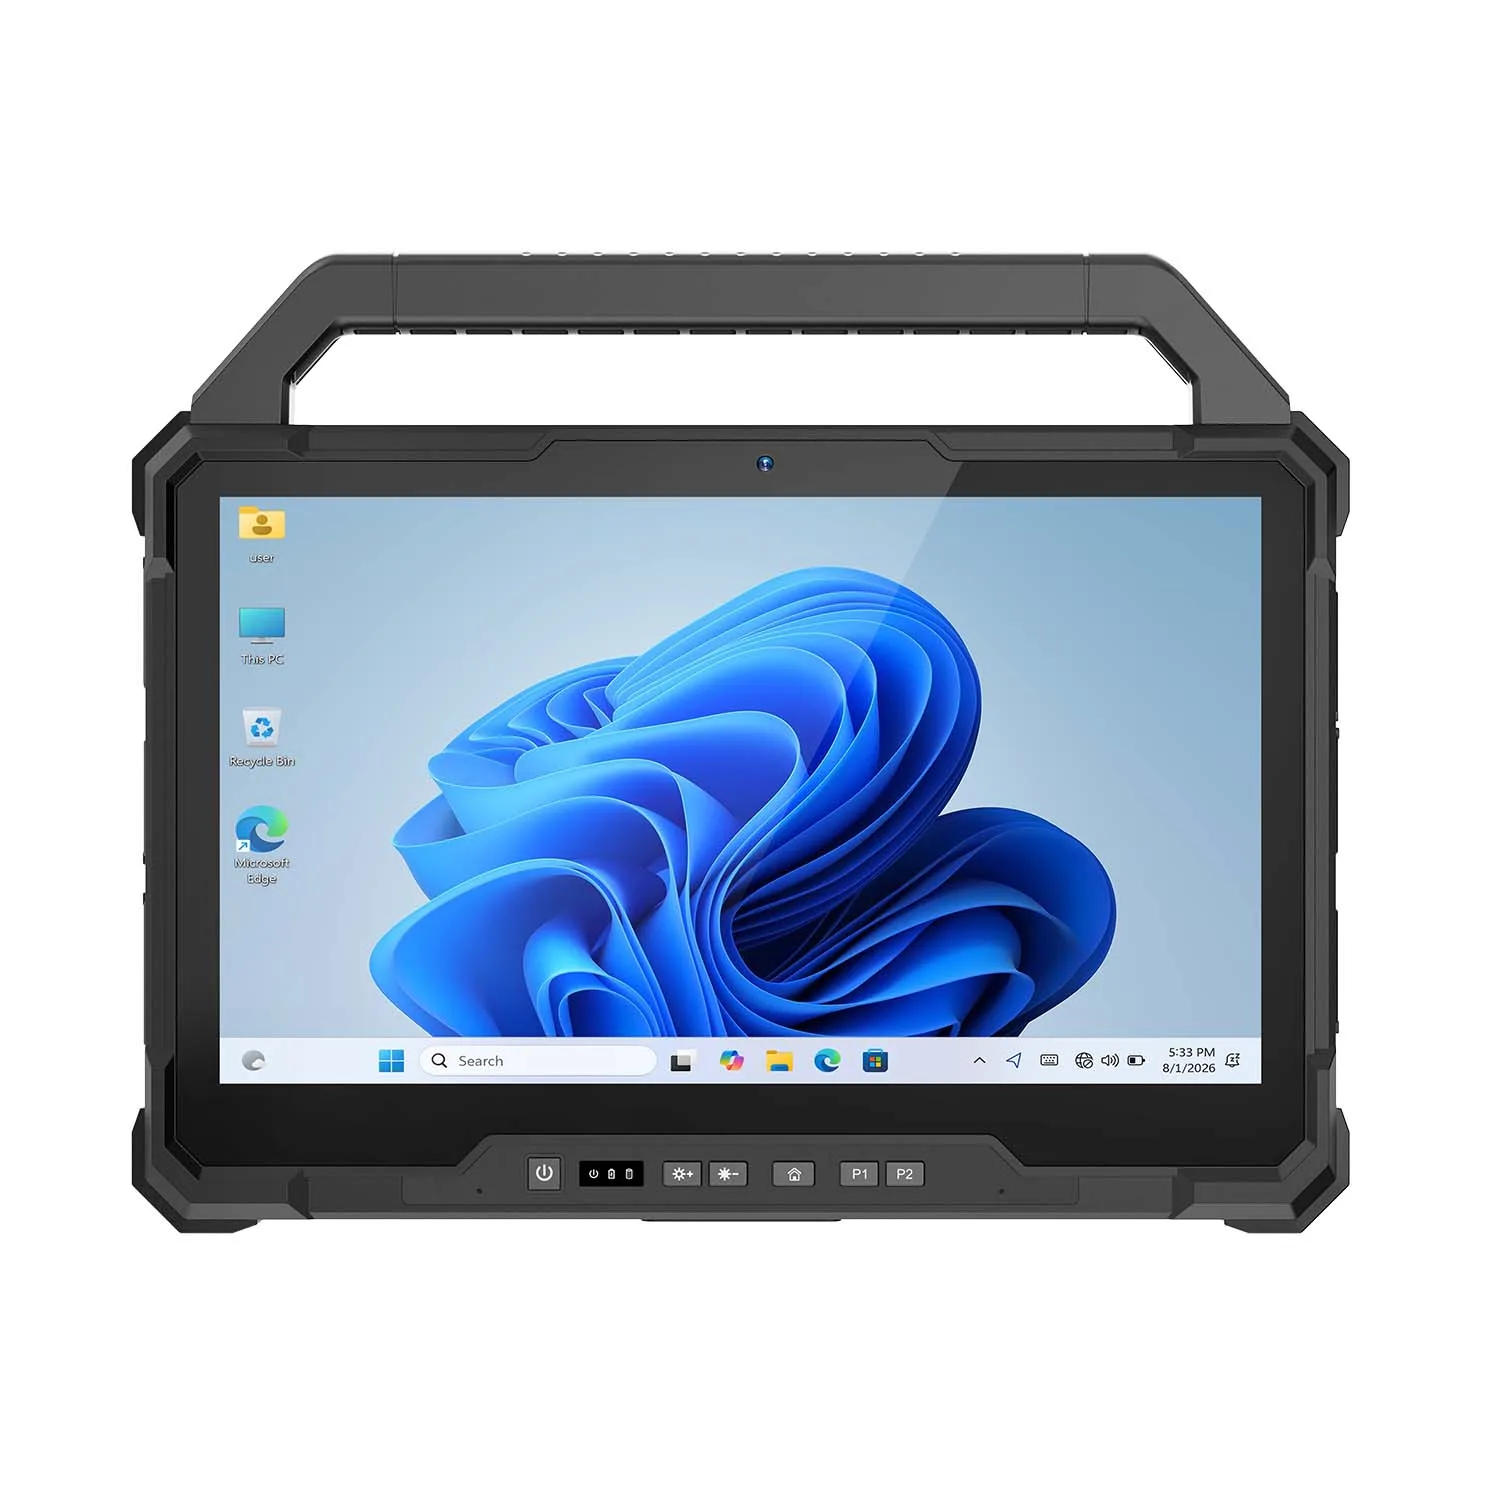
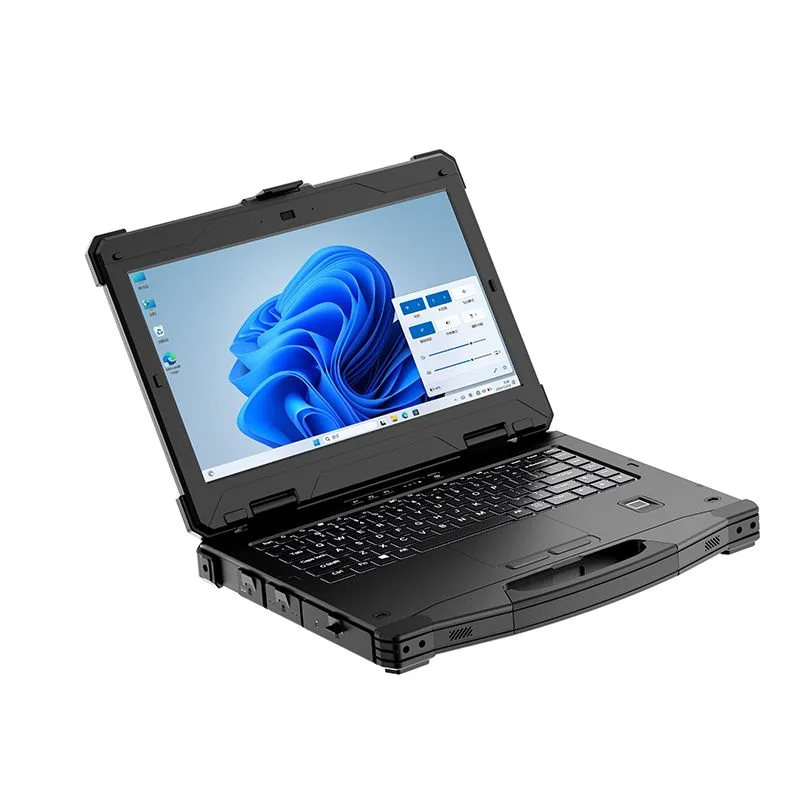
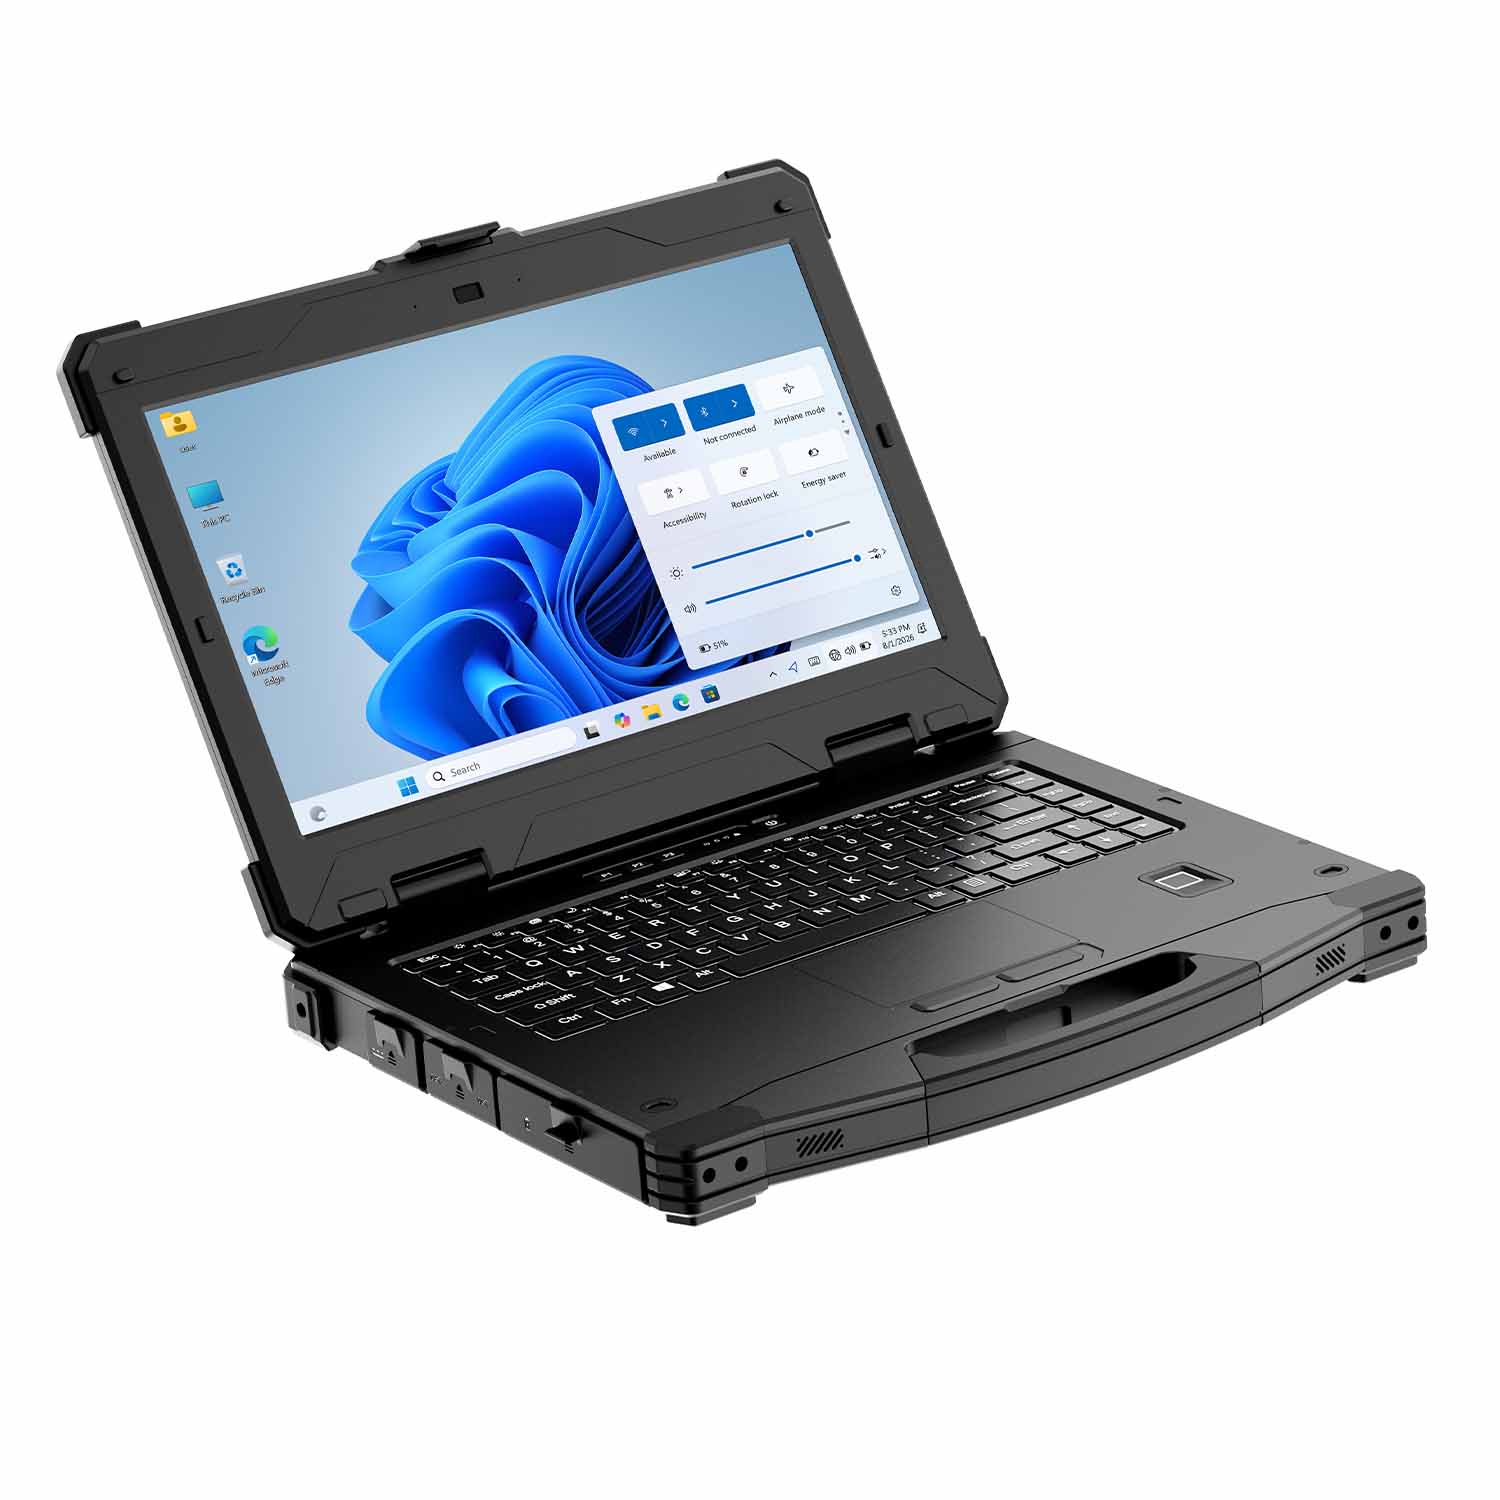
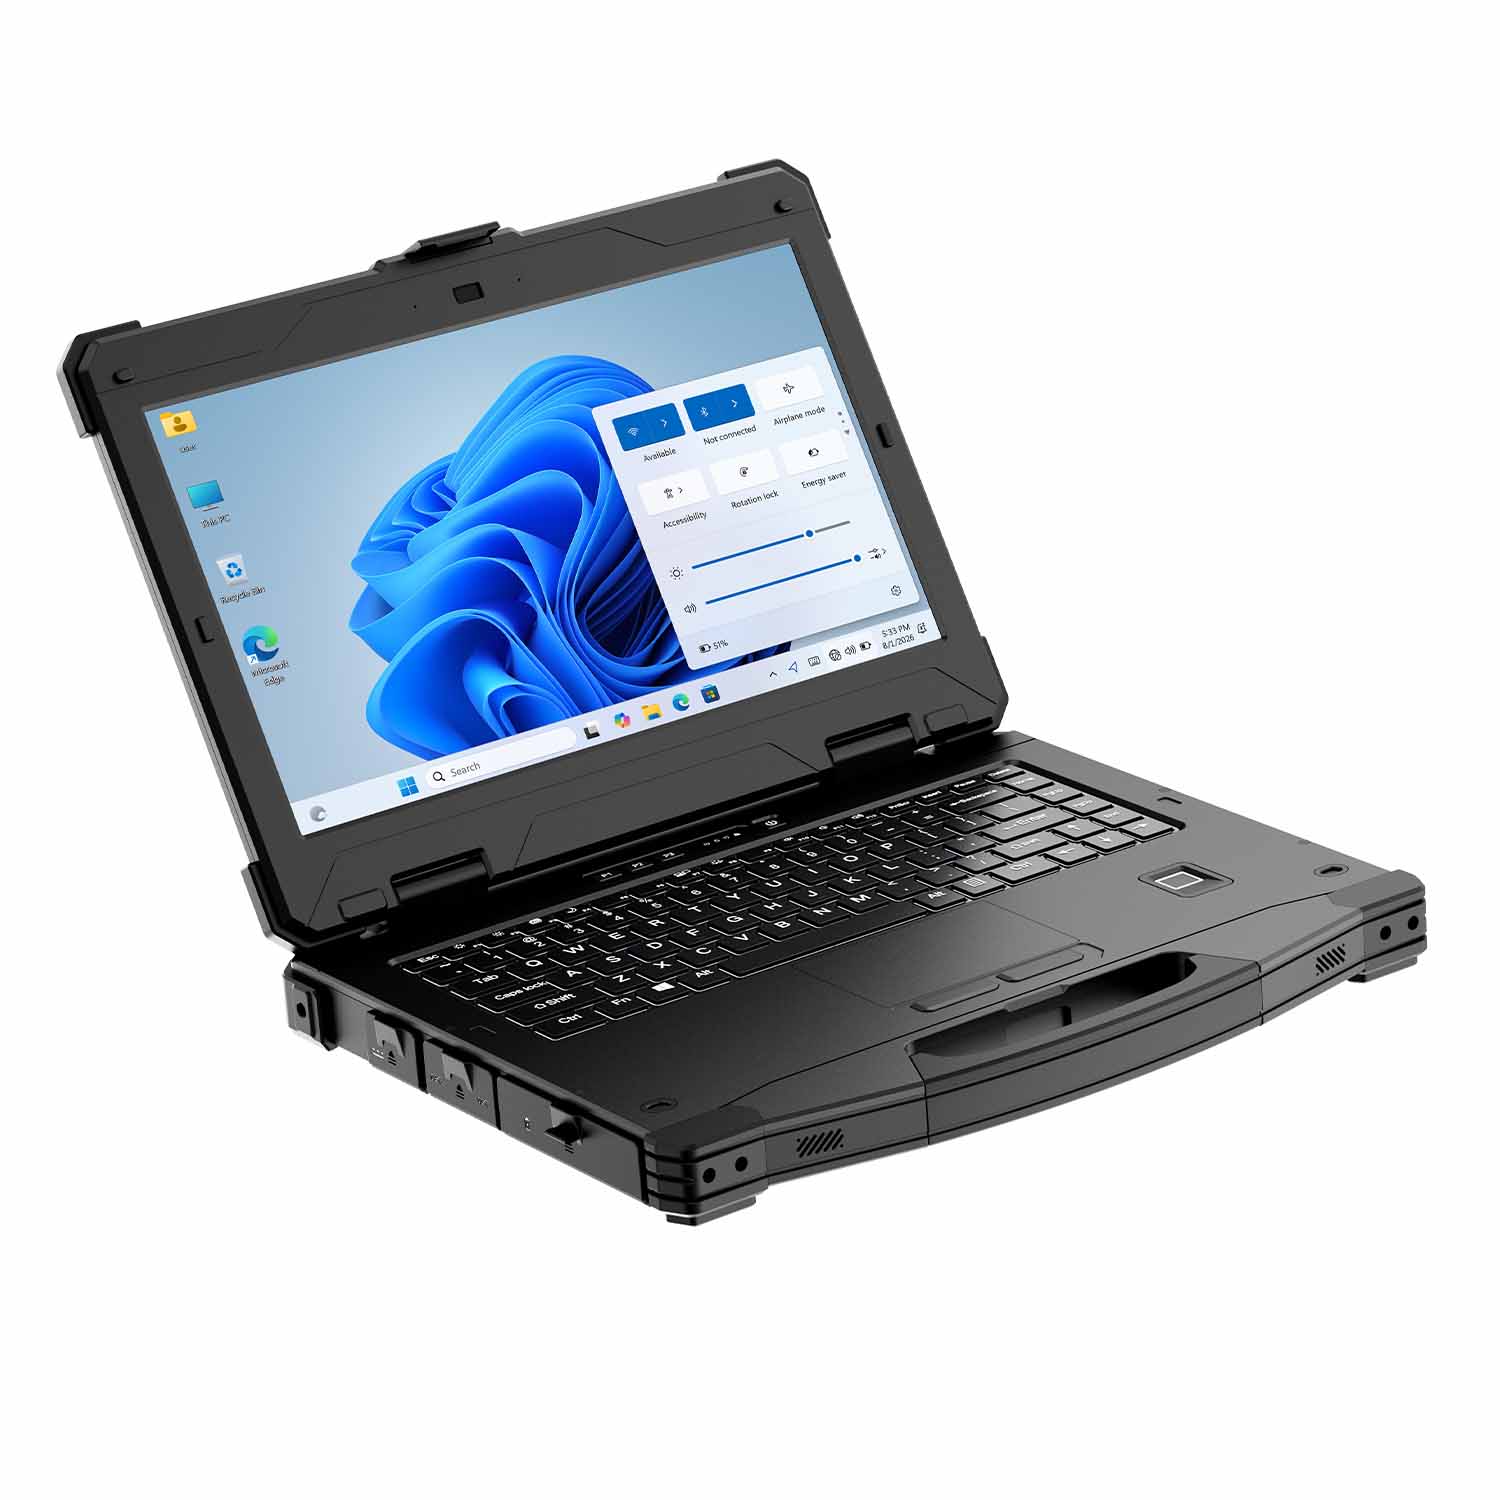
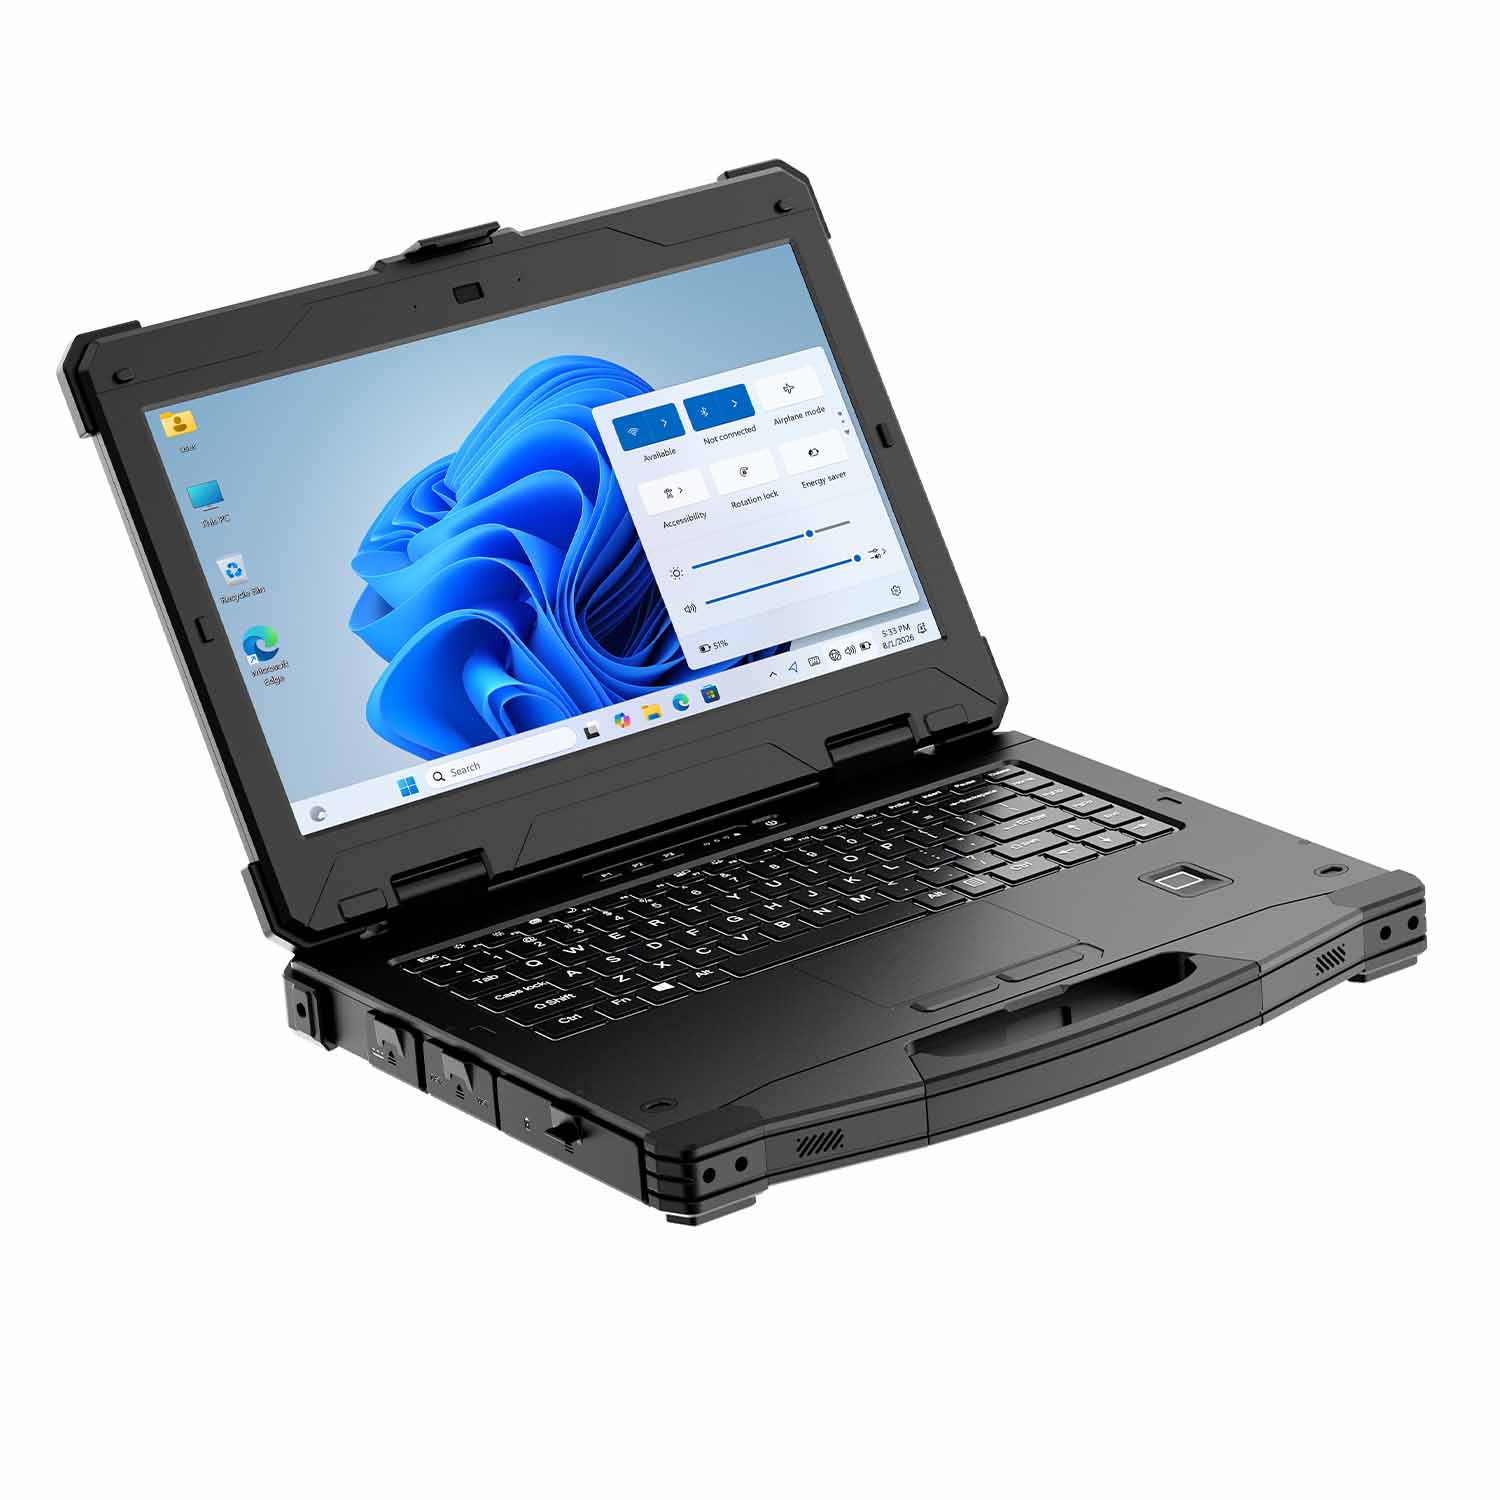
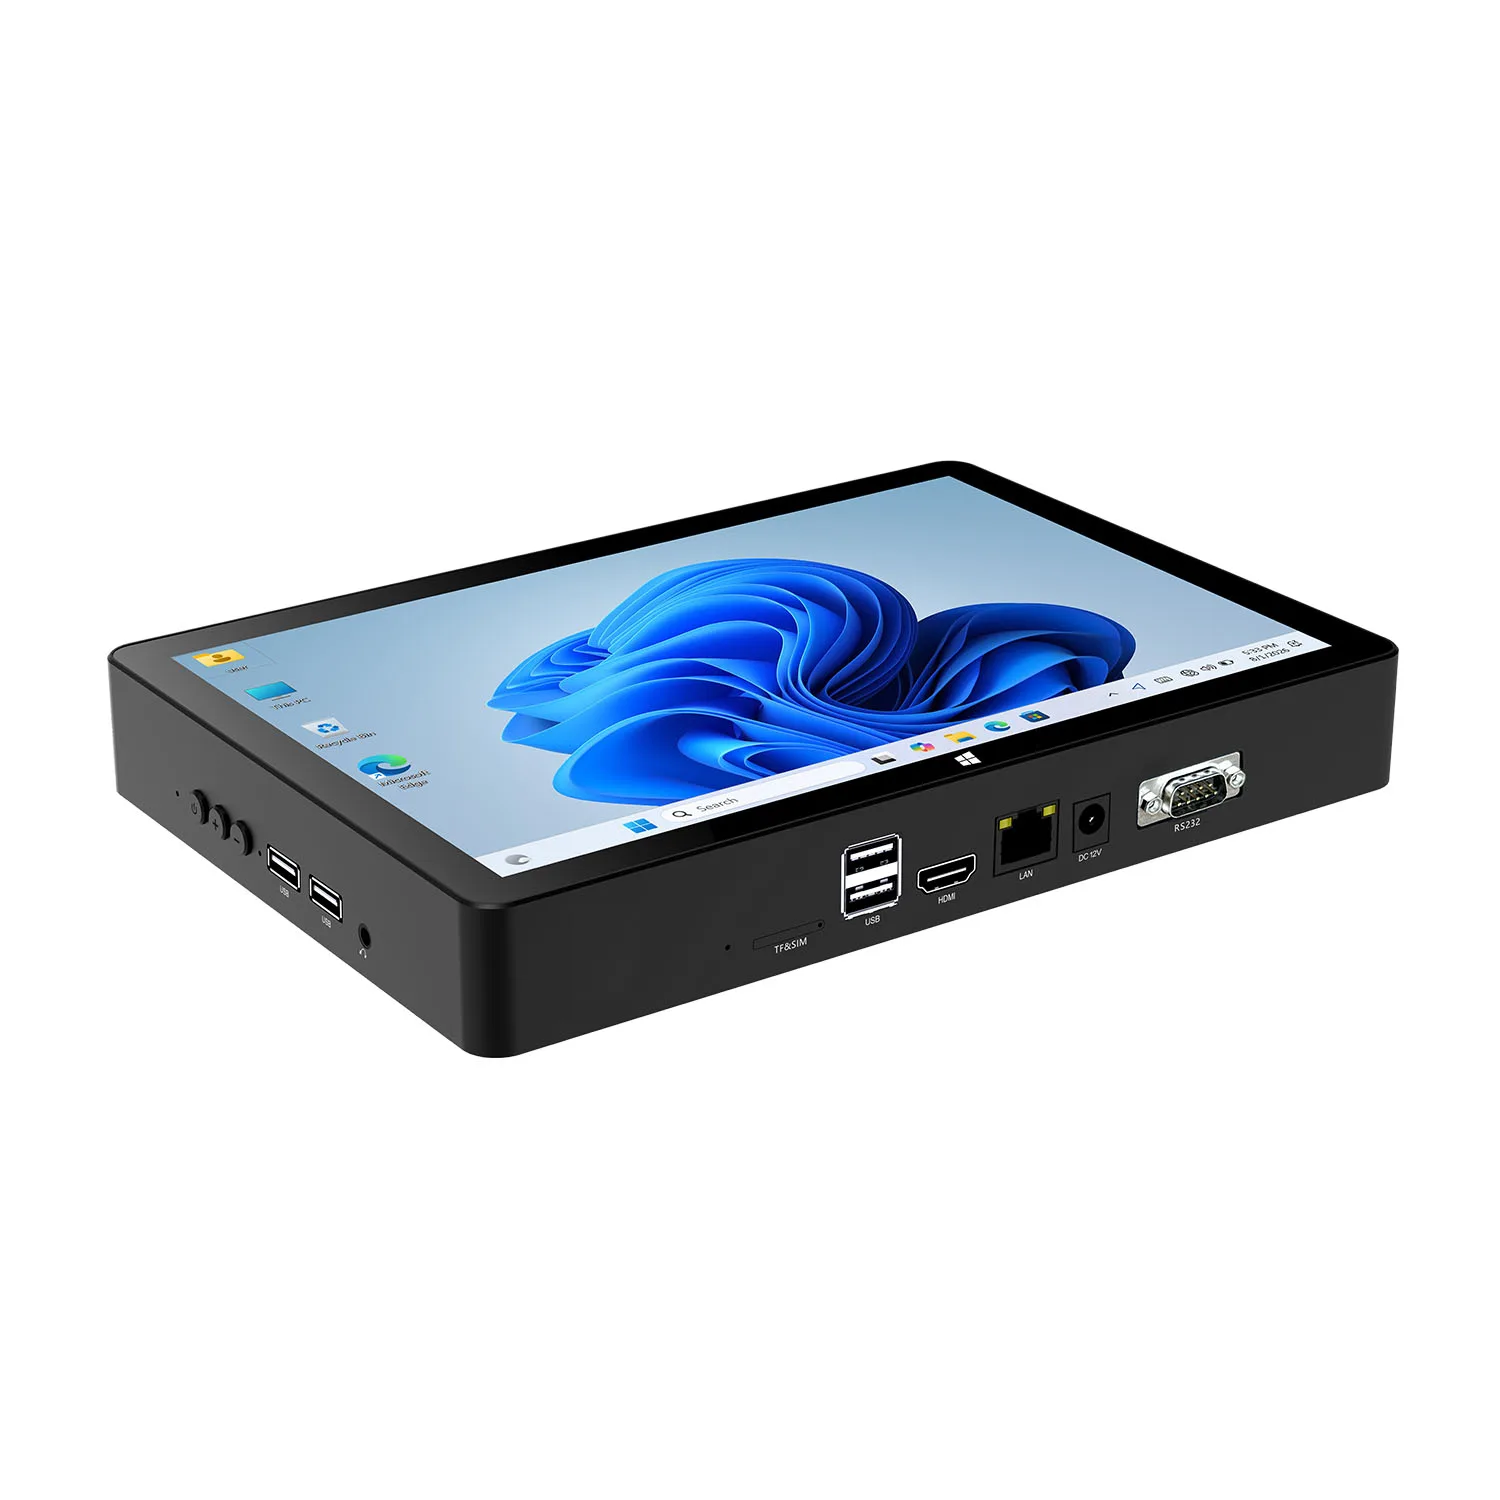
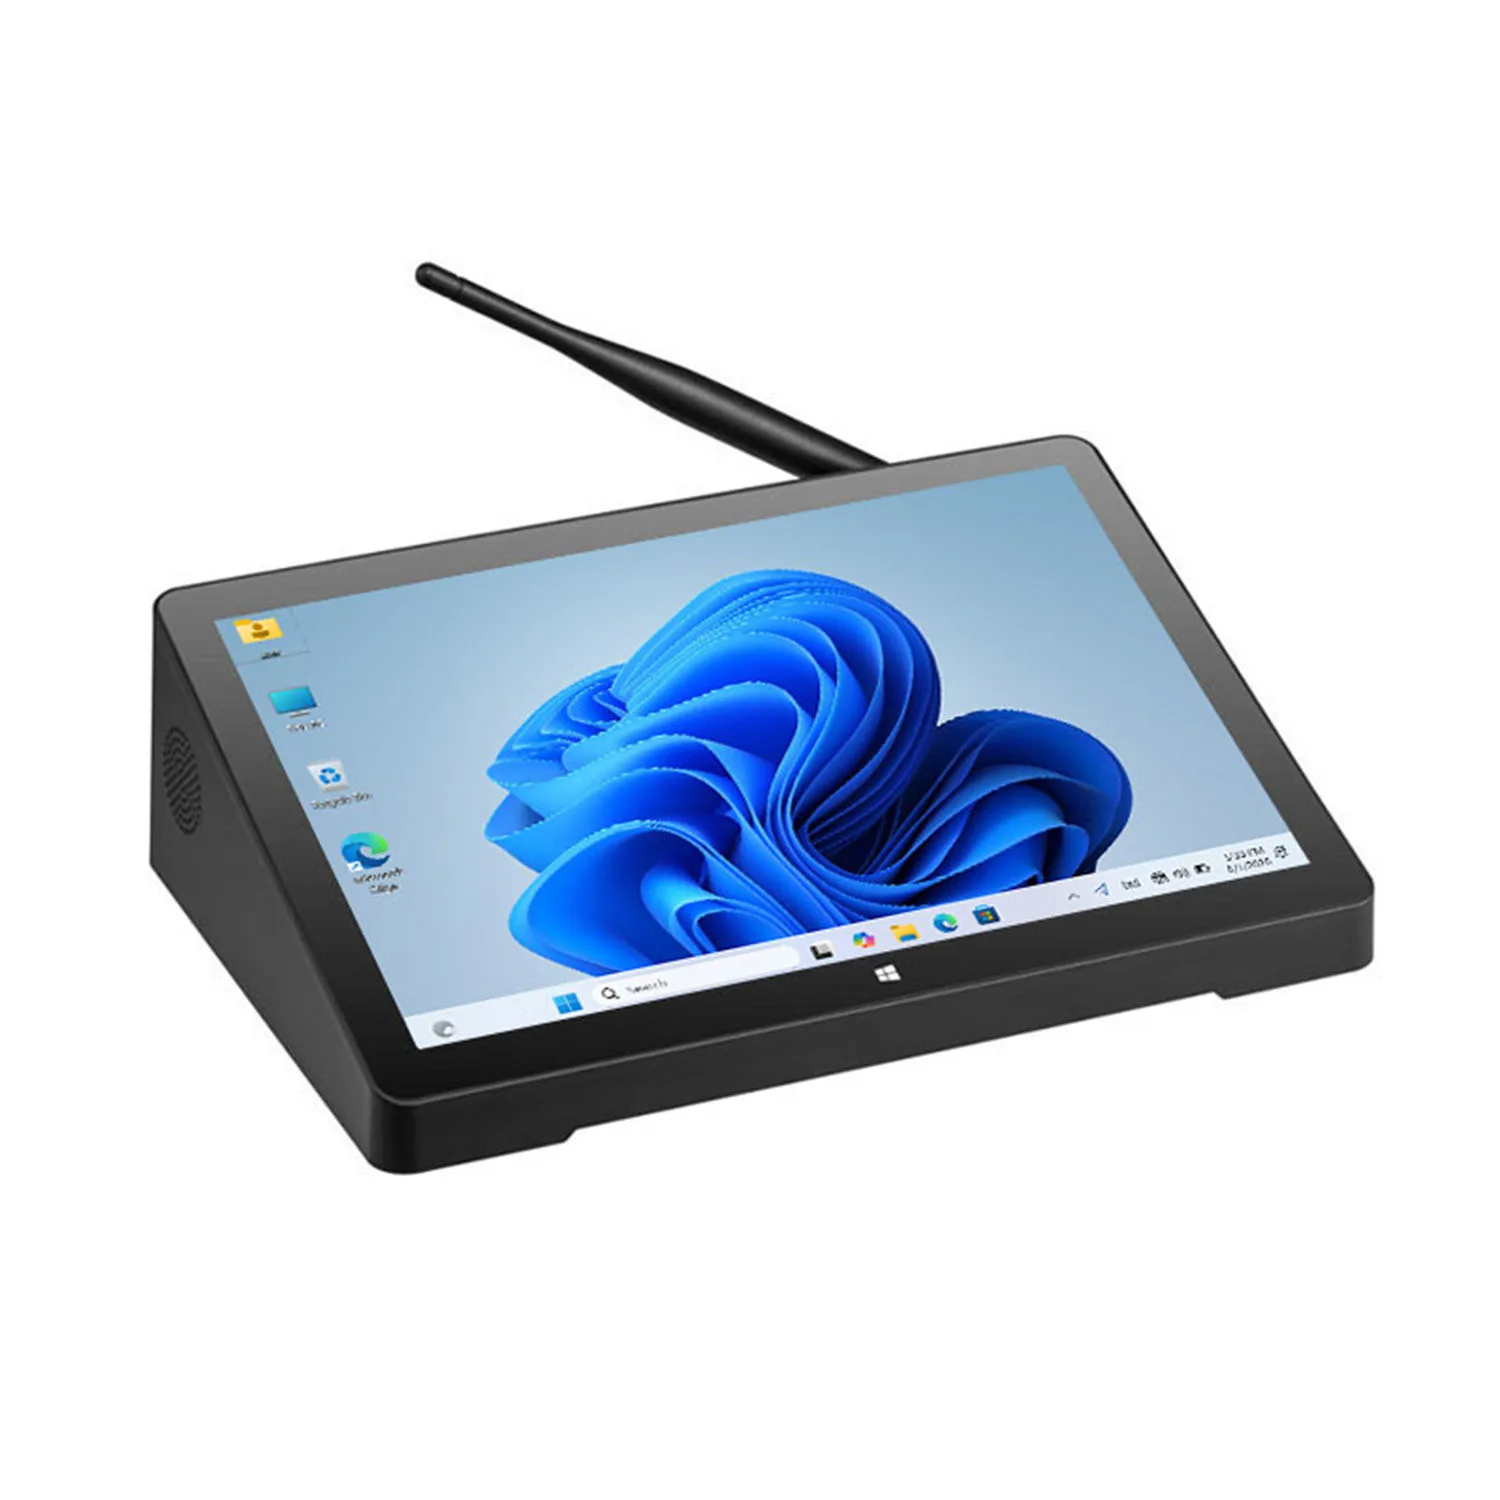
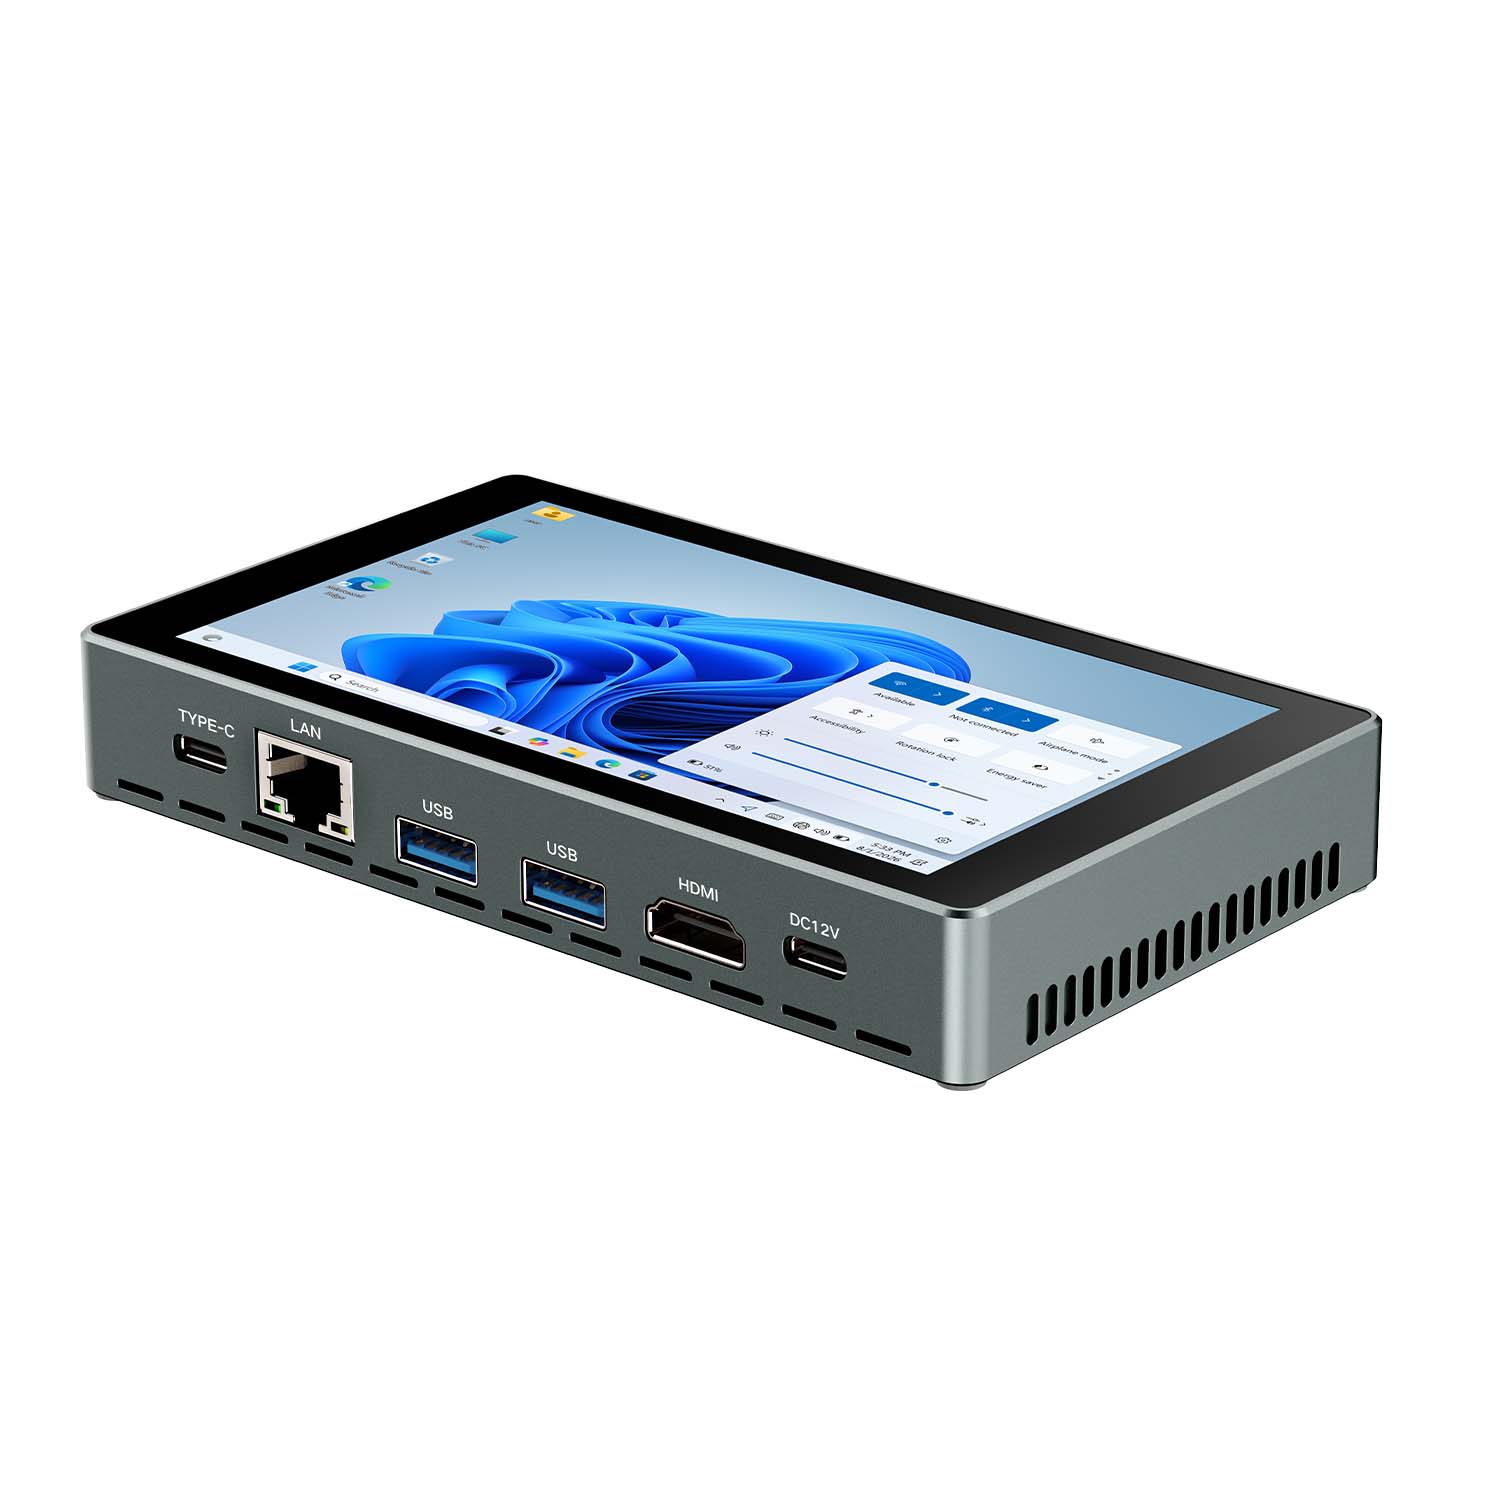
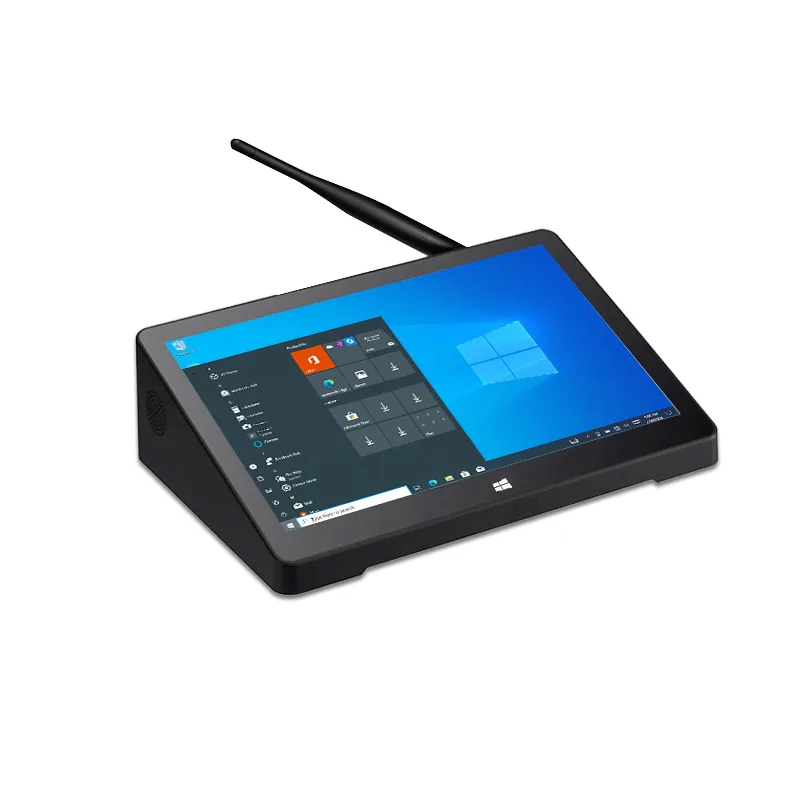
A factory floor kills office PCs. Dust clogs the fans, vibration loosens the connectors, and the shift never ends. CENAVA industrial panel PCs and rugged tablets run machine HMI, production monitoring, data collection and maintenance work in exactly those conditions — fanless, sealed, and rated for 24/7 duty.
Why Commercial Computers Struggle on the Factory Floor
Factory environments create operating conditions that consumer and office PCs are not normally designed to handle.
Metal dust, oil mist, machine vibration, temperature variation and continuous 24/7 operation can increase the risk of cooling problems, connector failures and storage-related faults. Systems installed beside CNC machines, stamping equipment, assembly lines or process machinery may also need to withstand frequent operator use and long production cycles.
An industrial computer failure can affect more than the computer itself. When the HMI goes dark, the line goes with it — operators lose alarm acknowledgement, production reporting stops, and work instructions disappear. So spec the computer for the floor, not the datasheet: protection rating, mounting, interfaces, OS compatibility and multi-year availability, in that order.
Industrial Computing Designed for Automation
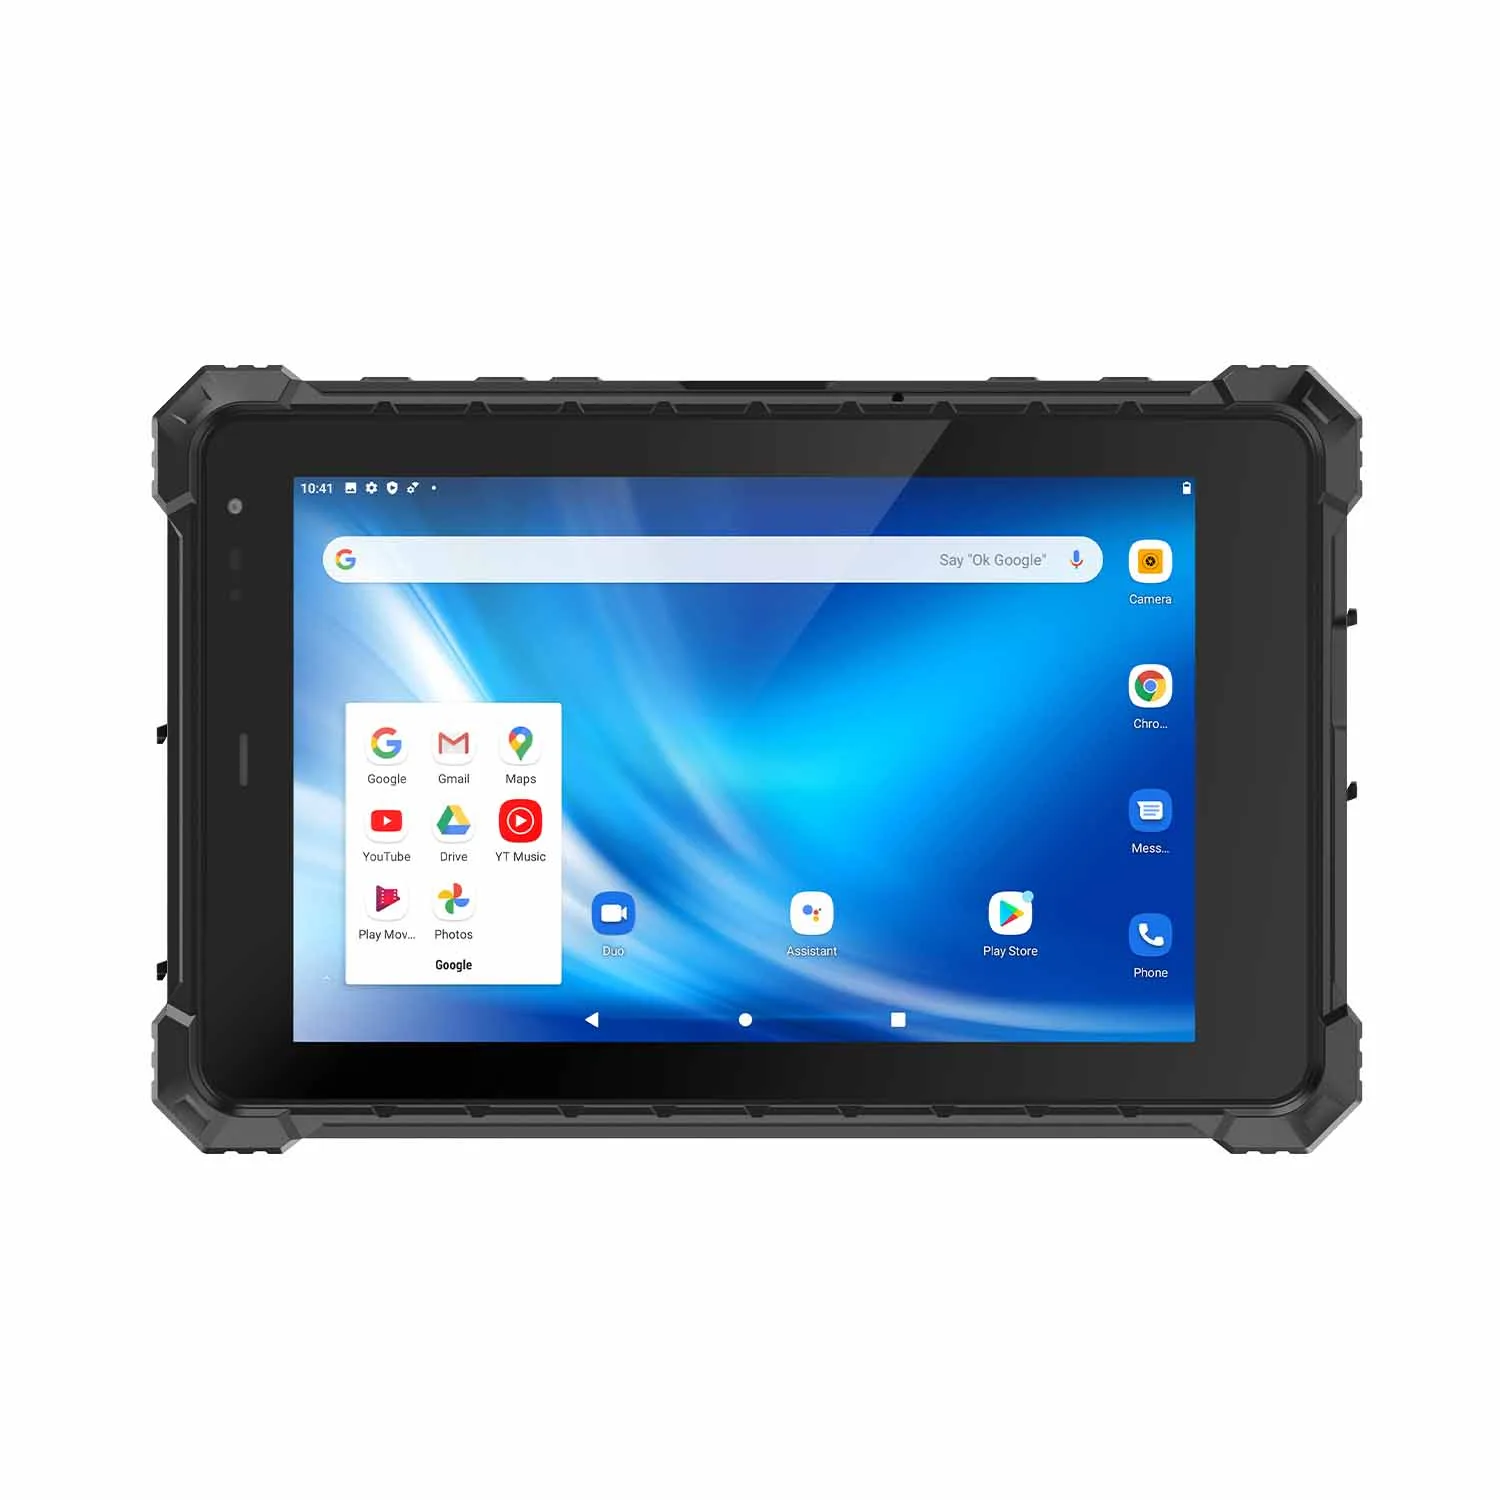
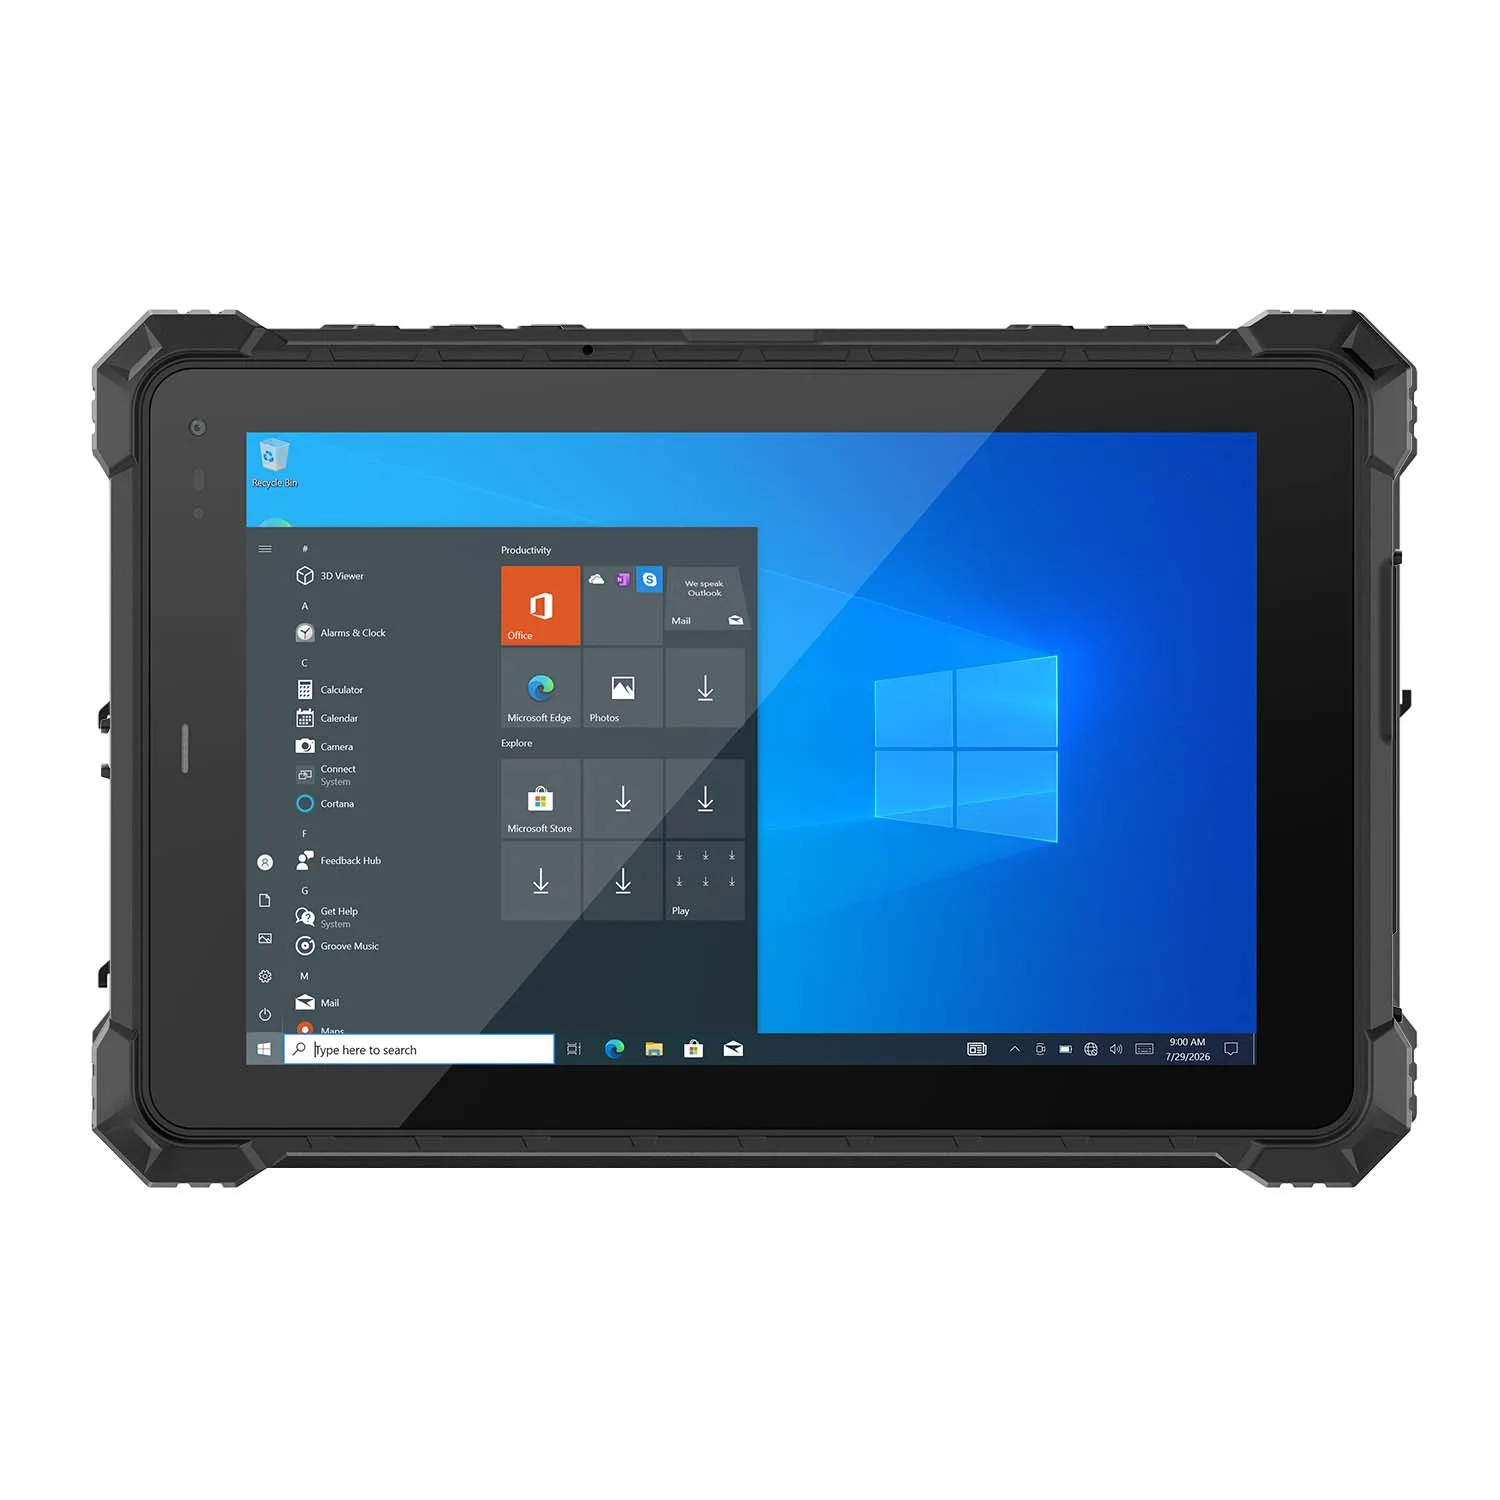
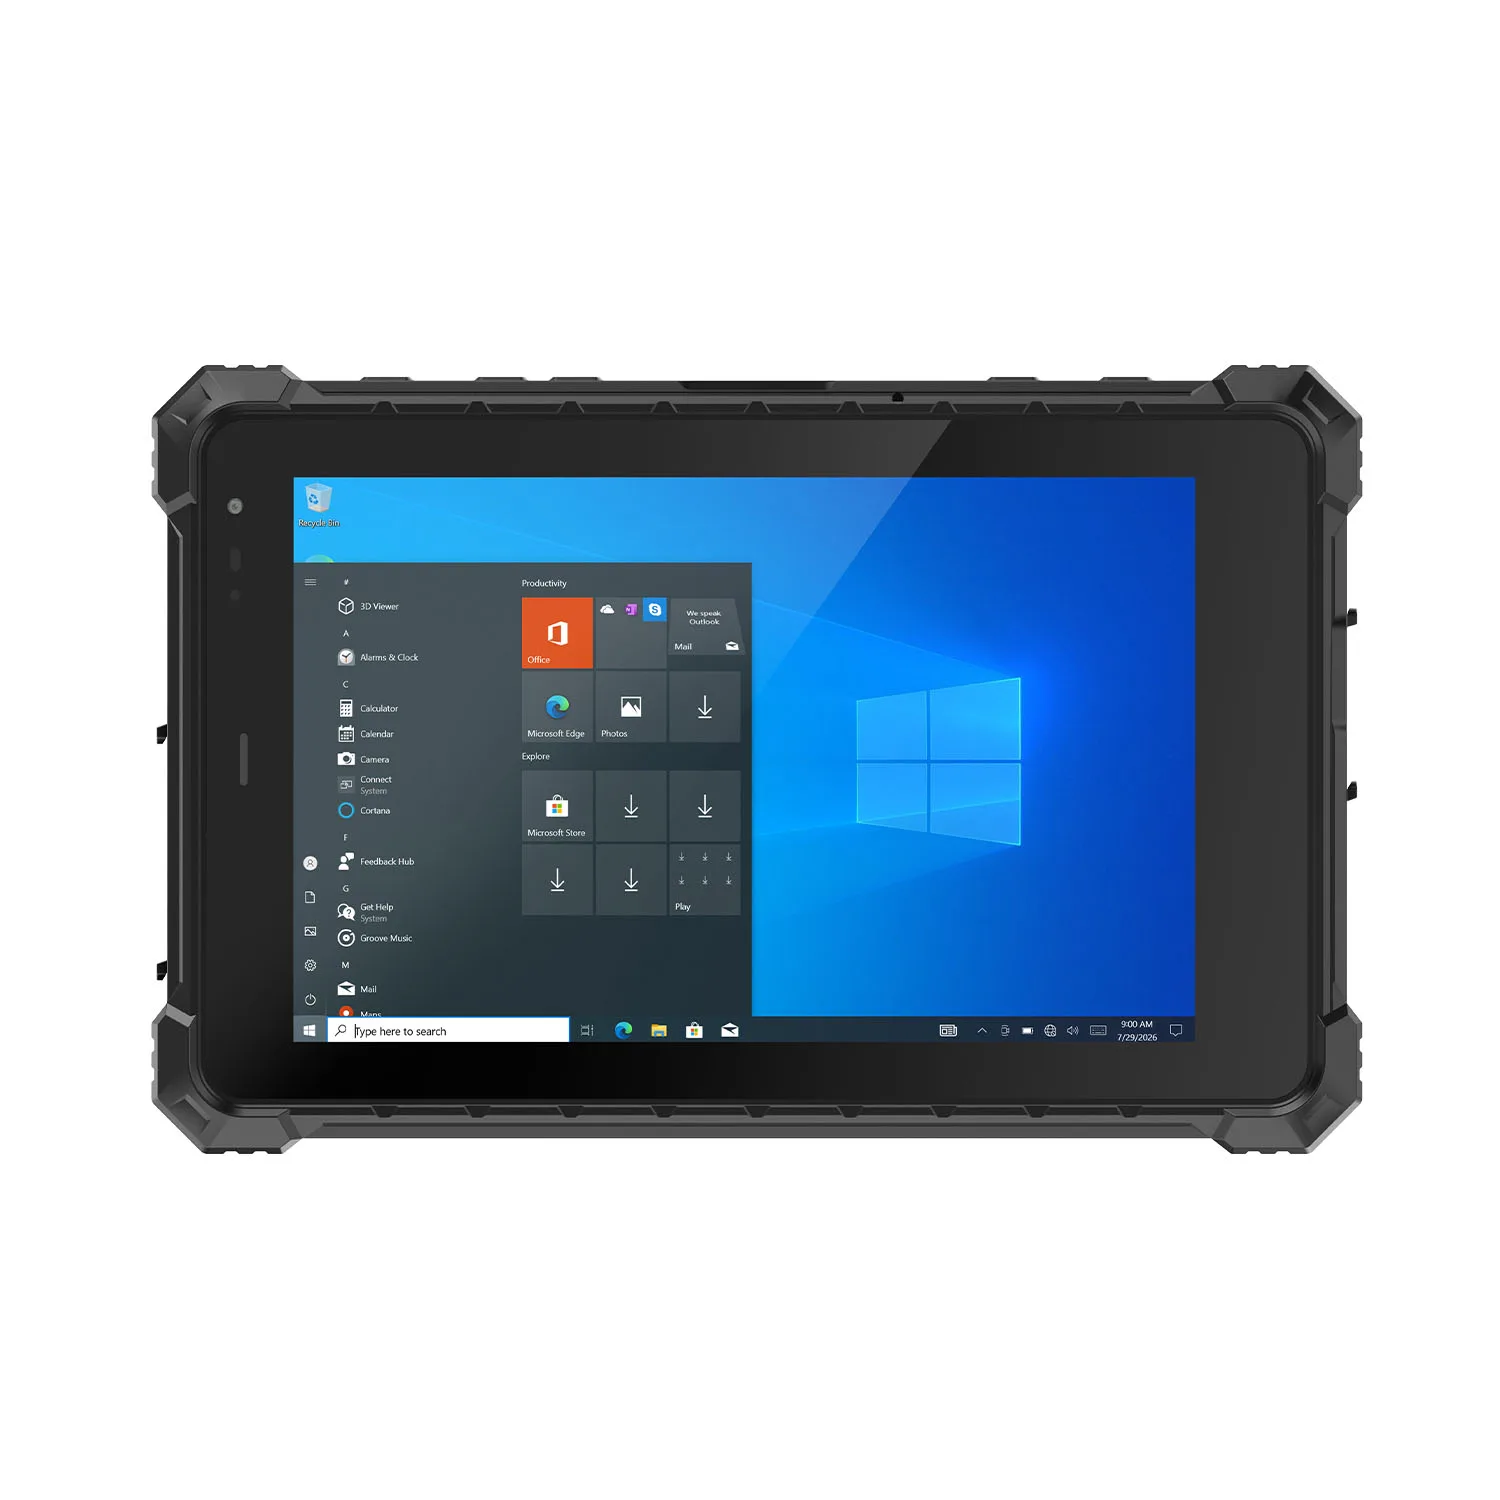
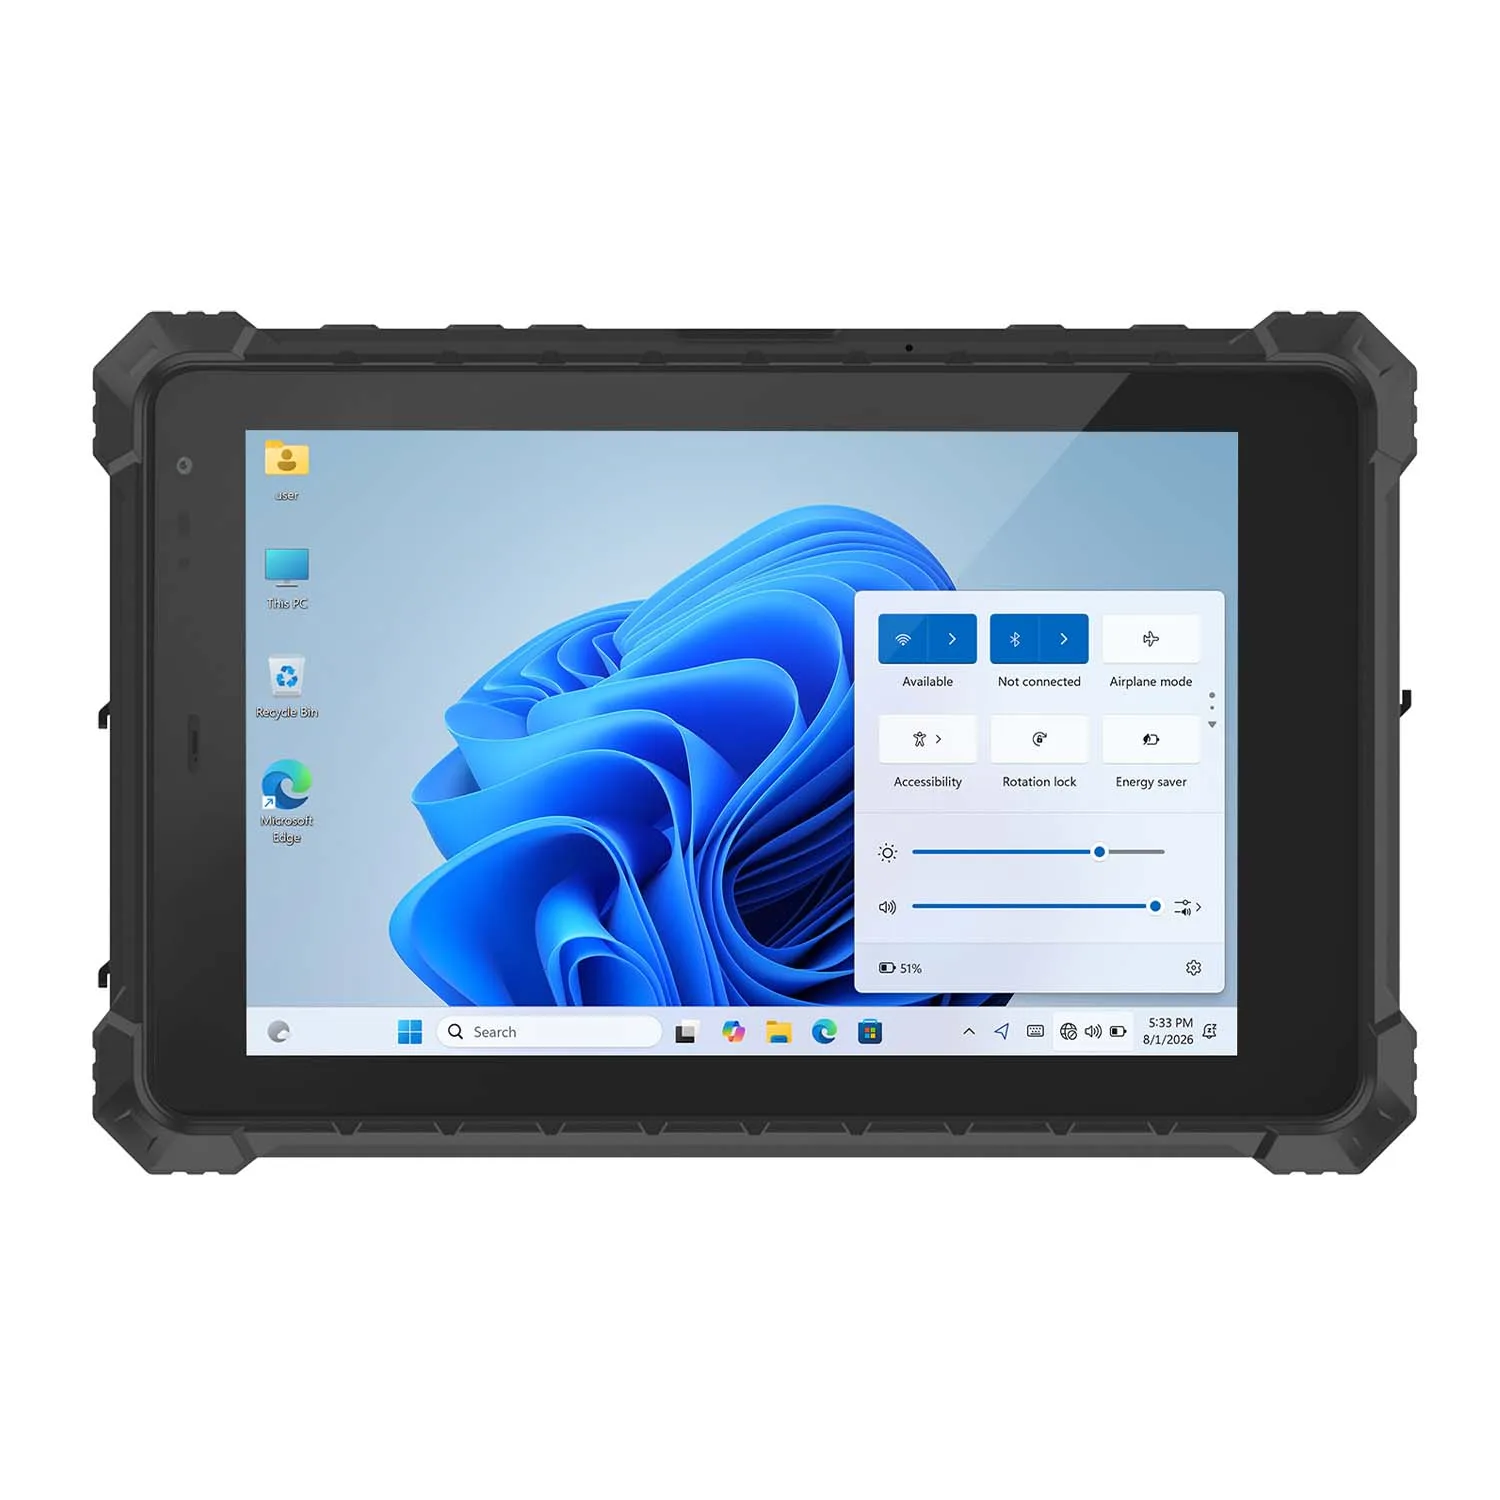
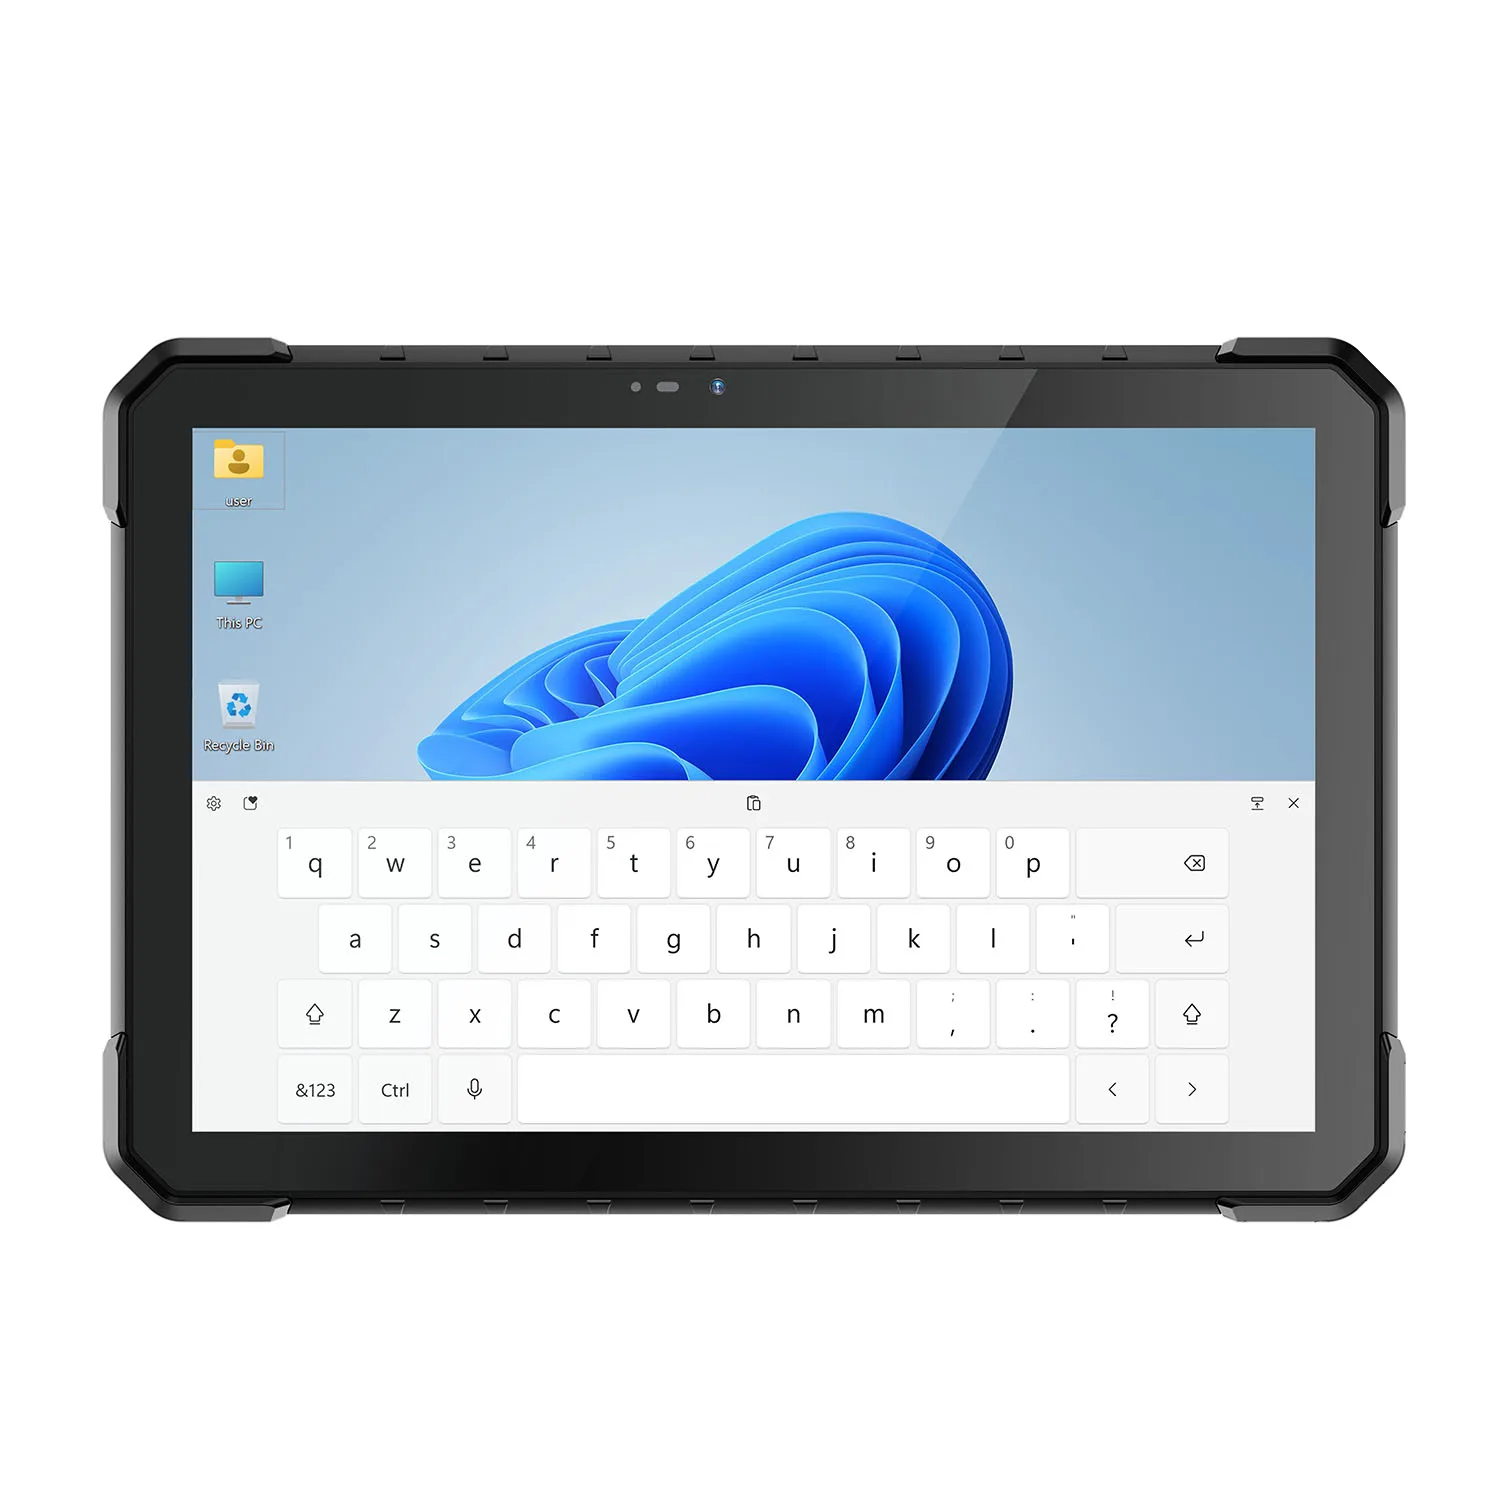
CENAVA provides industrial panel PCs and rugged tablets for fixed and mobile automation applications.
Fanless architectures help reduce airborne dust intake and eliminate cooling fans as a common mechanical maintenance point. Panel PCs in this range carry IP65-rated front panels — the operator-facing surface shrugs off dust and low-pressure washdown once the unit is seated correctly in the cutout. We rate the wide-temperature builds from -20°C to 60°C, which covers unheated warehouses in winter and cabinet interiors in July.
SSD storage and reduced internal cabling also help remove mechanical failure points associated with rotating hard drives and loose internal connections.
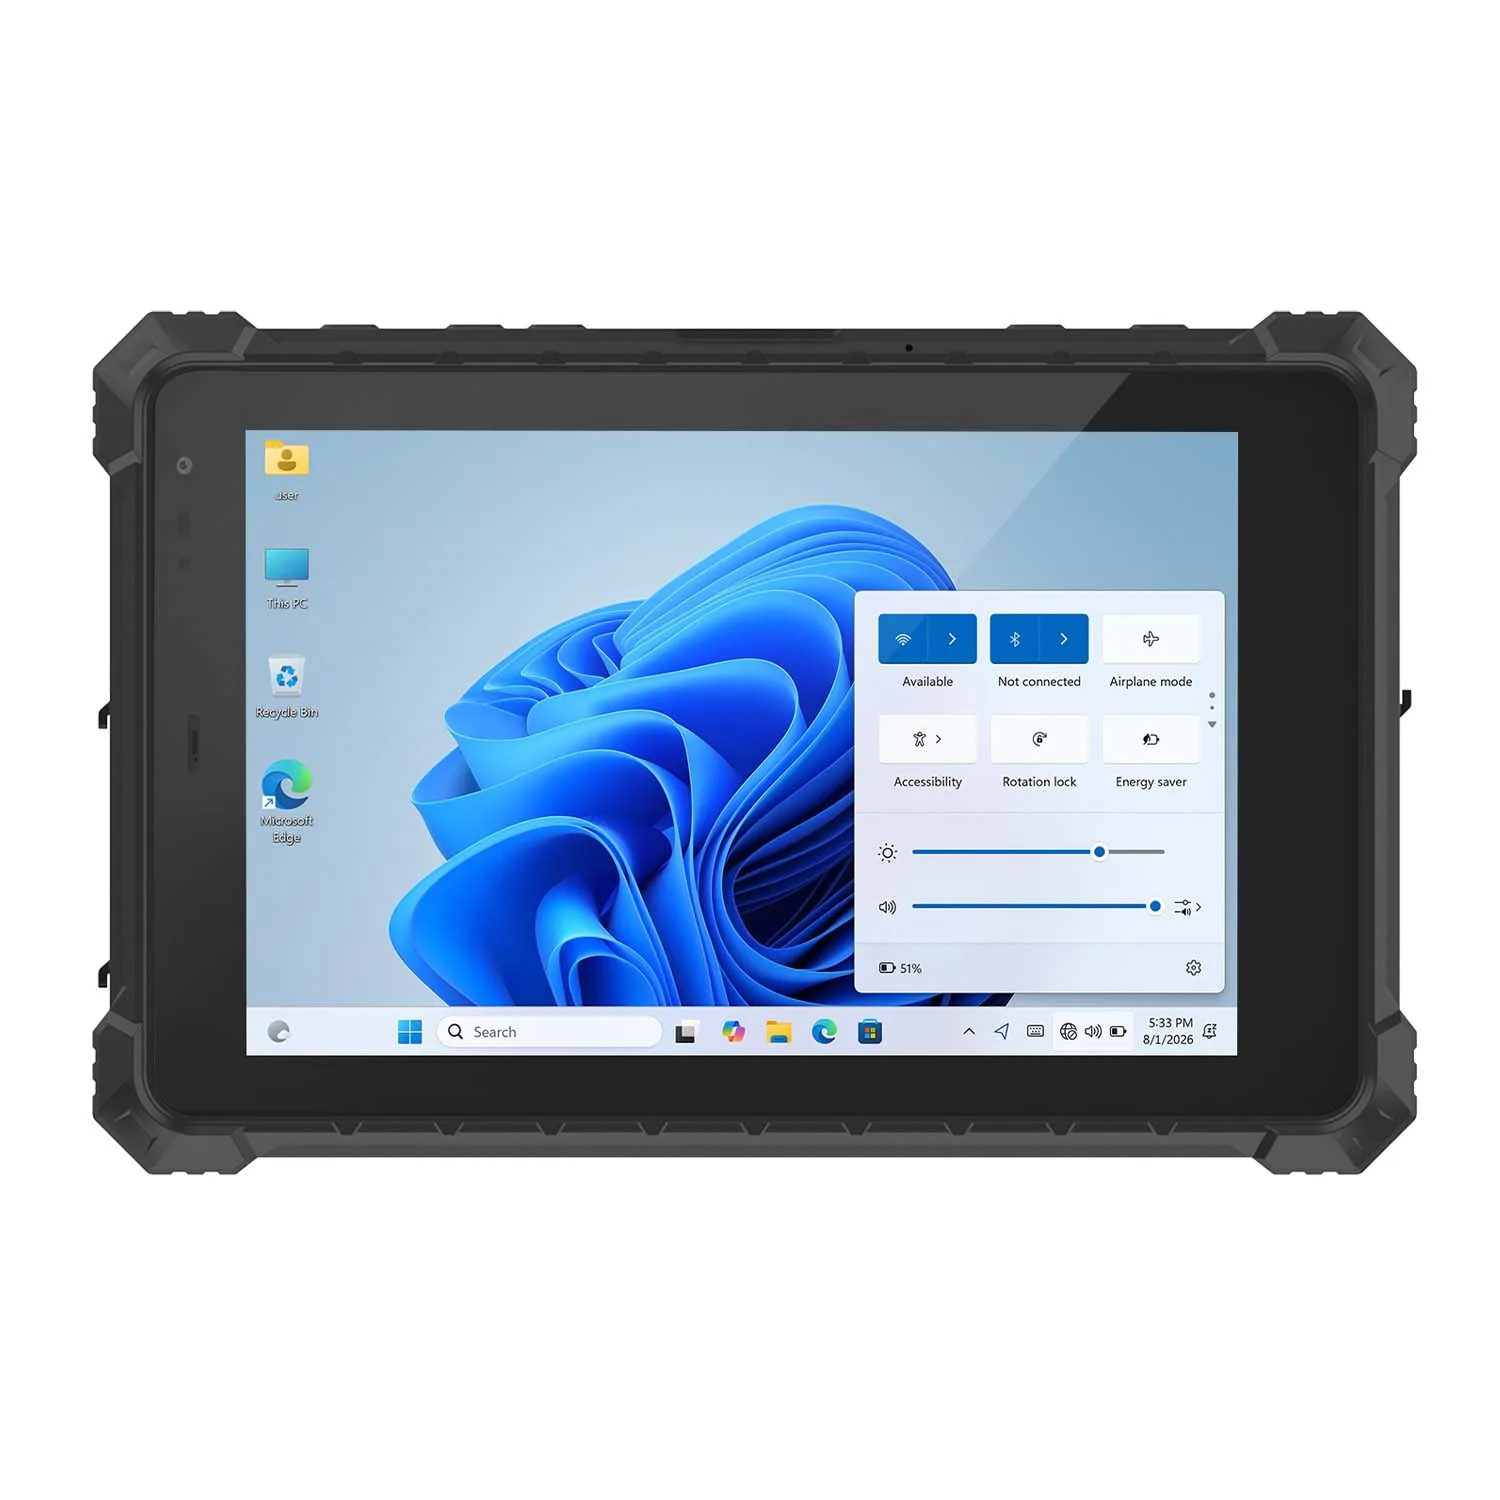
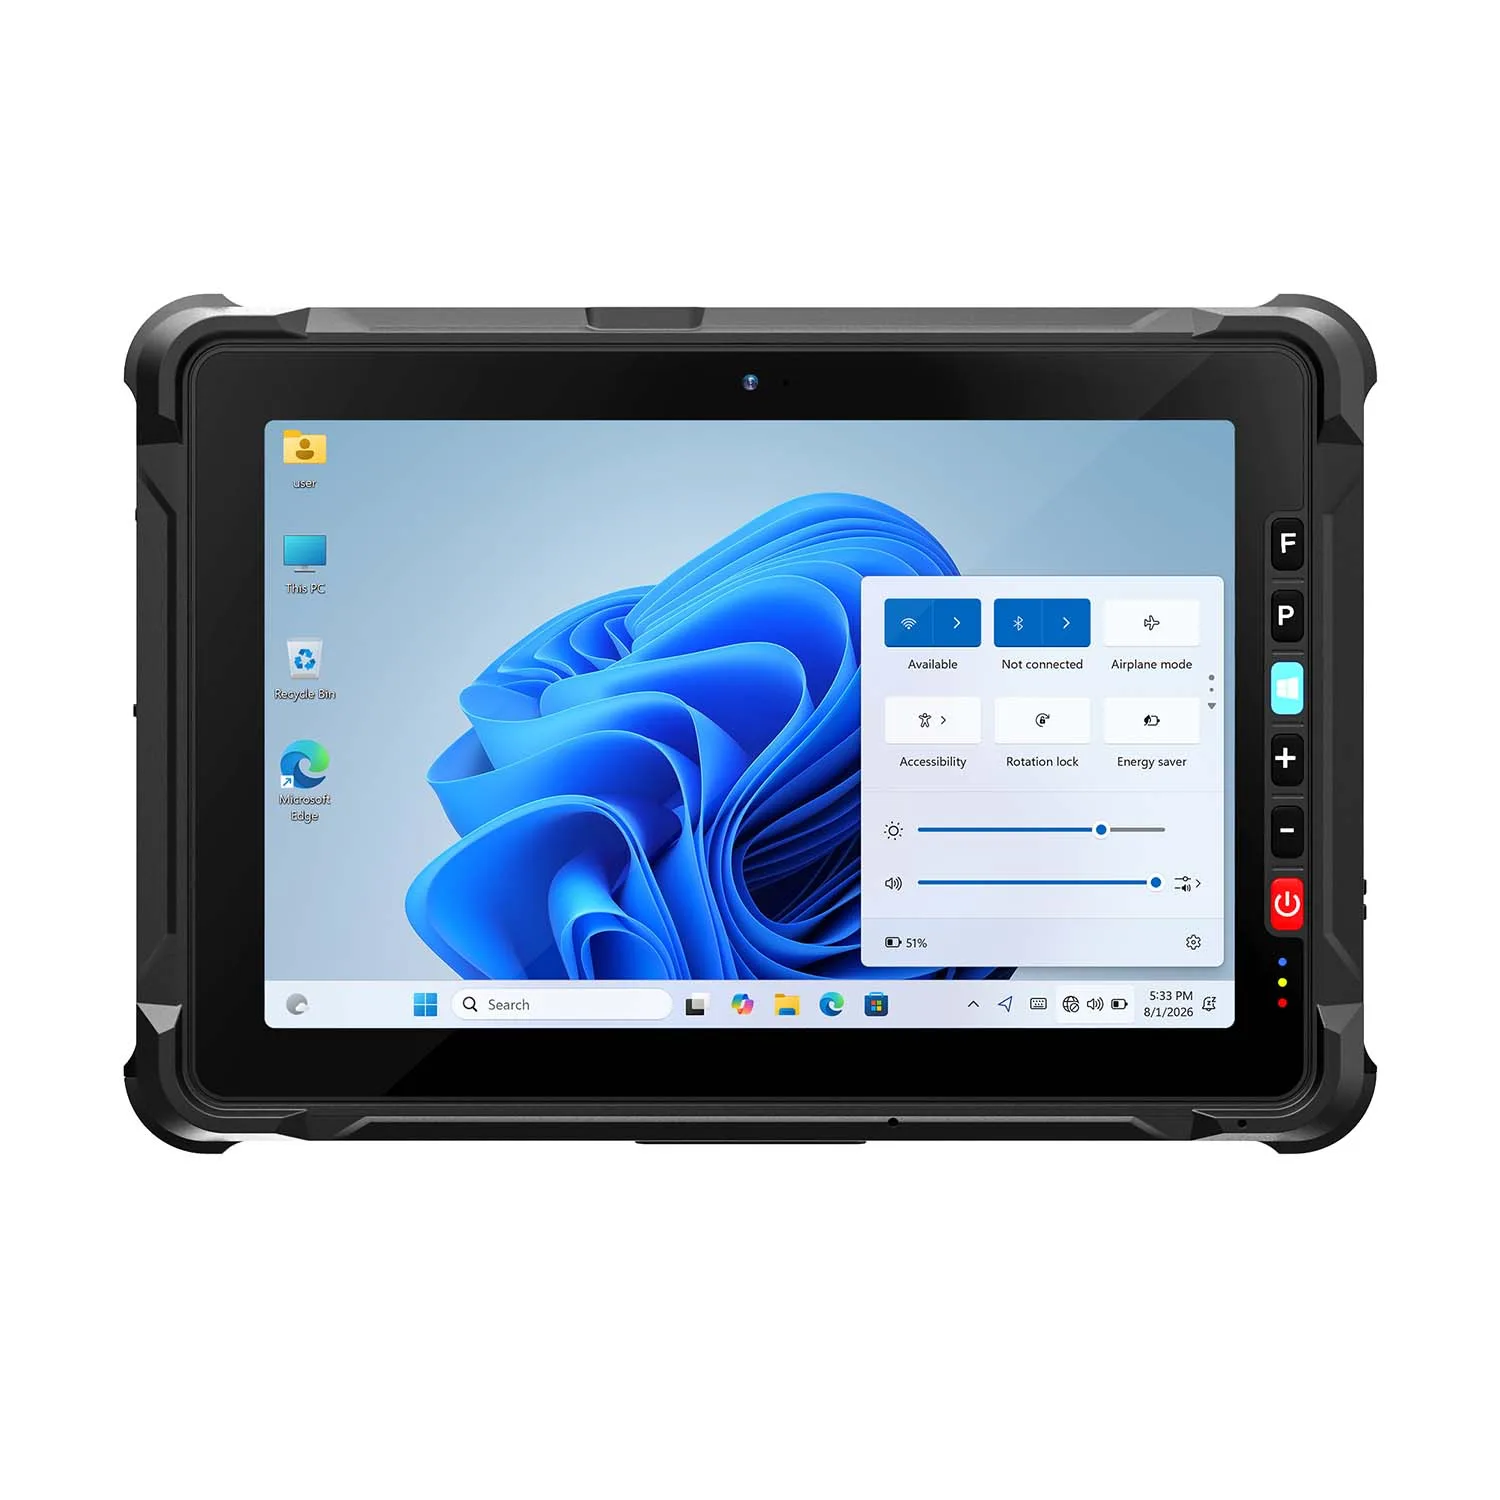
Different machines need different mounts. Panel-mount, VESA and wall-mount builds drop into machine enclosures, control cabinets and operator workstations. For mobile inspection, a rugged tablet puts production data in the technician's hand right at the machine — no walk back to a fixed terminal.
Industrial Automation Applications
Machine HMI and PLC Operation
An industrial panel PC acts as the operator's window into PLC-controlled equipment. On a typical machine it handles:
PLC status visualization
Machine alarm display
Recipe selection
Parameter adjustment
Production counters
Equipment status monitoring
Work-instruction display
A panel-mounted computer installed directly on a machine provides operators with a local interface while reducing the need for separate desktop equipment on the factory floor.
Legacy machinery is the reason serial ports still matter: plenty of PLCs, scanners and instruments on your floor talk RS-232, RS-422 or RS-485, and they will outlive the PC you mount next to them.
SCADA Operator Stations
Your SCADA station never sleeps. Industrial PCs in this role drive:
Real-time equipment monitoring
Alarm acknowledgement
Historical process data access
Equipment status visualization
Production trend monitoring
Process control interfaces
For SCADA duty, CPU is the easy part. Count the Ethernet ports first — dual GbE lets you keep machine traffic off the plant network — then check display size, OS compatibility, mounting location and how many years the platform stays orderable.
MES and Production Data Collection
MES only works when data entry happens at the station, not back at a desk. We mount the terminals right at the line, where they cover:
Work-order execution
Production reporting
Quality inspection
Product traceability
Barcode scanning
RFID workflows
Material tracking
Manual production data entry
A factory-floor MES terminal sits next to machinery and raw stock, not in an office. Match the enclosure, mounting, display protection and interfaces to the station it will actually live on — not to a generic spec sheet.
Andon and Shop-Floor Terminals
The same hardware doubles as an Andon terminal or production information board. It shows:
Production status
Line performance
Downtime reasons
Quality alerts
Maintenance requests
Production targets
Operator instructions
A local shop-floor terminal can also provide operators with a convenient data-entry point for downtime reporting, quality checks or production confirmation.
Fixed Panel PCs and Rugged Tablets in the Same Production Environment
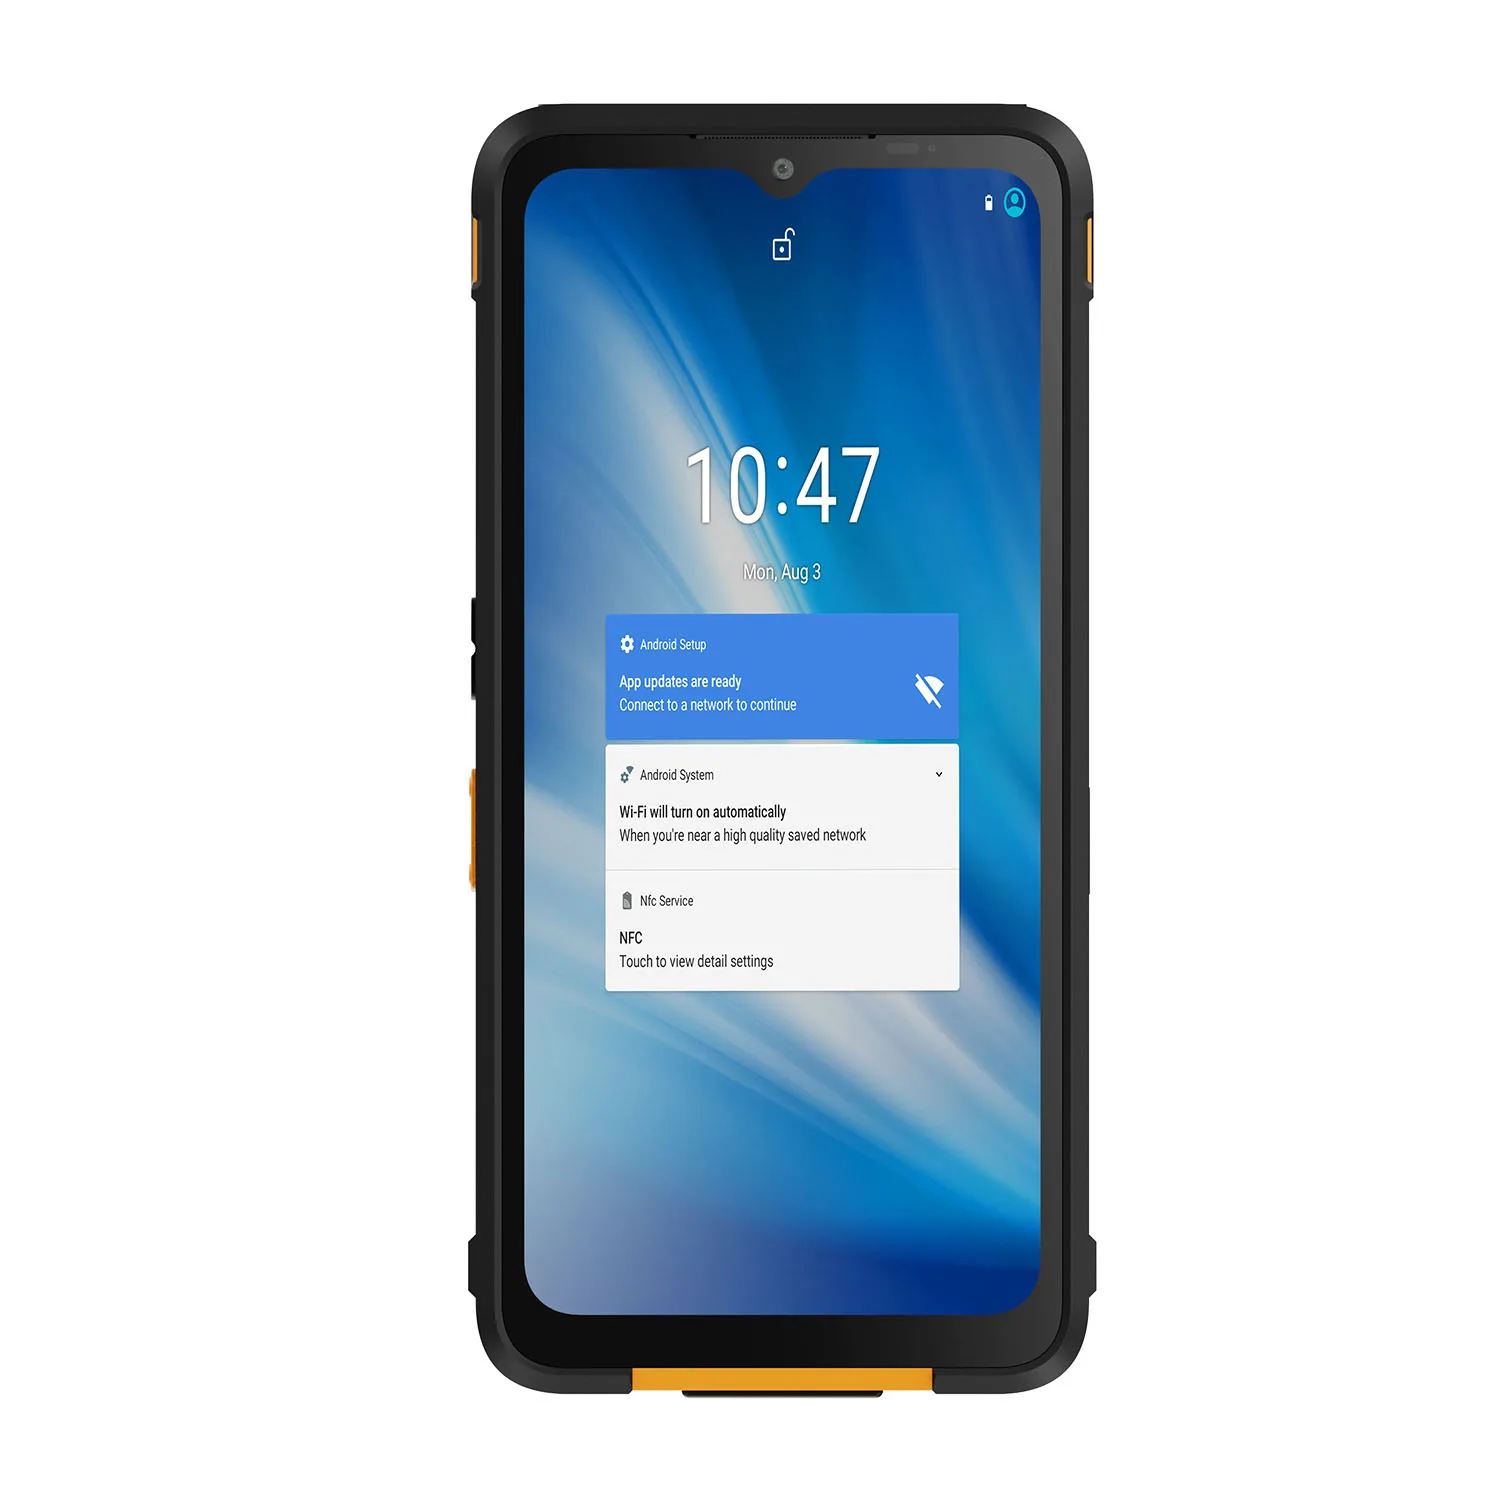
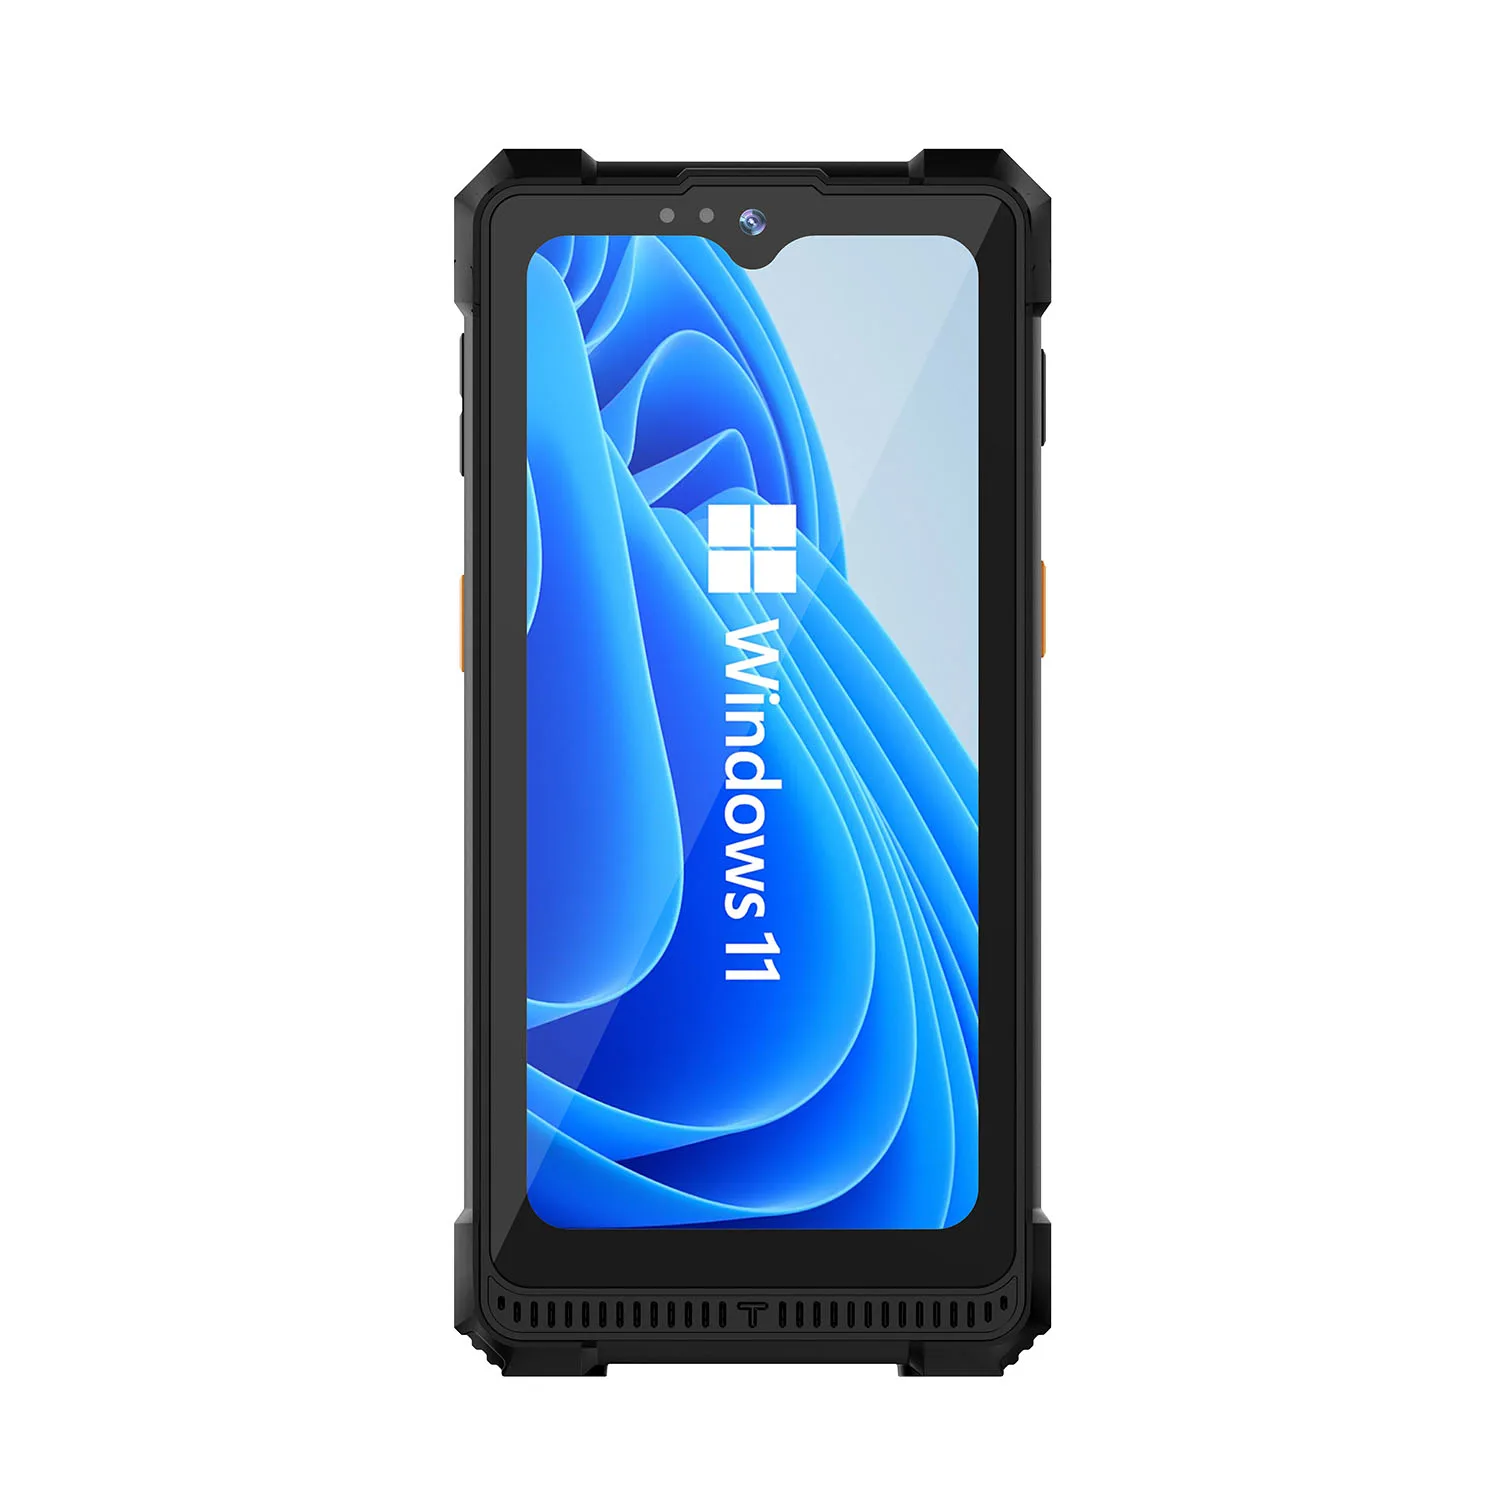
One production line, two kinds of computer. The fixed panel PC runs the machine HMI; a rugged tablet goes with the maintenance technician.
For example, a technician may use a rugged Windows tablet to review PLC diagnostics, equipment documentation, maintenance records or MES work orders beside the machine while the fixed panel PC continues to provide the operator interface.
Each covers the job the other can't reach.
How to Select an Industrial Computer for Automation
The best industrial computer is not necessarily the system with the highest processor specification.
Selection should begin with the operating environment and automation requirements.
1. Identify the Installation Environment
Consider where the computer will operate.
Weigh these before anything else:
Dust exposure
Oil mist
Water exposure
Machine vibration
Ambient temperature
Continuous operating hours
Indoor or semi-outdoor installation
A panel PC mounted beside production equipment may require a protected front surface and fanless cooling, while a computer installed inside a protected control cabinet may place greater priority on connectivity and long-term component availability.
2. Confirm the Mounting Method
Three ways to mount them:
Panel mounting
VESA mounting
Wall mounting
Machine-frame mounting
Measure the cutout first. Mounting dimensions decide the shortlist when you replace an existing HMI or build a computer into a machine enclosure — send us the panel drawing and we will match it.
3. Check PLC and Peripheral Interfaces
Automation projects often require a combination of modern and legacy interfaces.
Per model and build sheet, I/O options cover:
RS-232
RS-422
RS-485
Dual Gigabit Ethernet
CAN
USB
GPIO
Lock the interface list before production. Every external converter added later is more wiring, more cost, and one more failure point in the cabinet.
4. Verify Operating-System and Software Compatibility
Hardware selection should also consider the software environment.
Match the OS image to what your line actually runs:
HMI software
SCADA clients
MES applications
PLC programming tools
Machine-vision software
Barcode or RFID applications
Custom manufacturing software
Ask us to verify drivers for everything you plan to plug in — scanners, printers, PLC interfaces, cameras and any specialized peripherals. We test them on the target OS image before the units ship.
5. Consider Product Lifecycle Before CPU Performance
Industrial equipment often remains in service much longer than consumer IT hardware.
A CPU upgrade that improves benchmark performance may provide little benefit if it forces a customer to revalidate software, drivers, mounting dimensions or peripheral compatibility several years later.
For long-term automation projects, platform availability and controlled BOM management can therefore be as important as processor performance.
Industrial I/O for Factory Integration
A commercial PC gives you USB and one LAN port. A factory needs more. CENAVA systems ship with RS-232/422/485, Ethernet, CAN and GPIO per build sheet.
The serial ports keep talking to:
Legacy PLCs
Barcode scanners
Measurement instruments
CNC equipment
Industrial printers
Existing production machinery
Ethernet handles modern PLC communication, SCADA networks, MES links and plant-level data exchange. Define the interface set from the machine architecture — not from whatever adapters happen to be in the toolbox after installation.
Long-Term Hardware Availability
Industrial automation equipment may remain in production for many years.
Frequent changes to computer hardware can create additional engineering work because a replacement platform may require:
Software revalidation
Driver testing
Mechanical redesign
I/O changes
Image deployment changes
Customer requalification
CENAVA supports long-term product availability and controlled BOM management to help reduce unnecessary redesign risk in industrial automation projects.
Need the platform for five years or more? Say so at selection time, and we will put the availability period in the quotation.
OEM and ODM Industrial Computer Services
Off-the-shelf hardware doesn't fit every machine builder or integrator — that's why we run OEM and ODM programs. Customization covers:
BIOS configuration
Custom branding
Housing customization
I/O pinout and connector placement
Operating-system configuration
Software image pre-installation
Hardware configuration adjustments
On volume runs, fixing these details before mass production means less installation work at your customer's site and identical hardware across every machine and location.
Manufacturing and Compliance
Industrial computing projects may require different regulatory and compliance requirements depending on the destination market and application.
Selected CENAVA products are designed to meet applicable CE, FCC and RoHS requirements.
Production is managed under an ISO 9001:2015-certified quality management system. A copy of the certificate is available on request and is included in our standard RFQ response package.
Tell us the destination market, and we will state the CE, FCC and RoHS status of your exact configuration in the quotation.
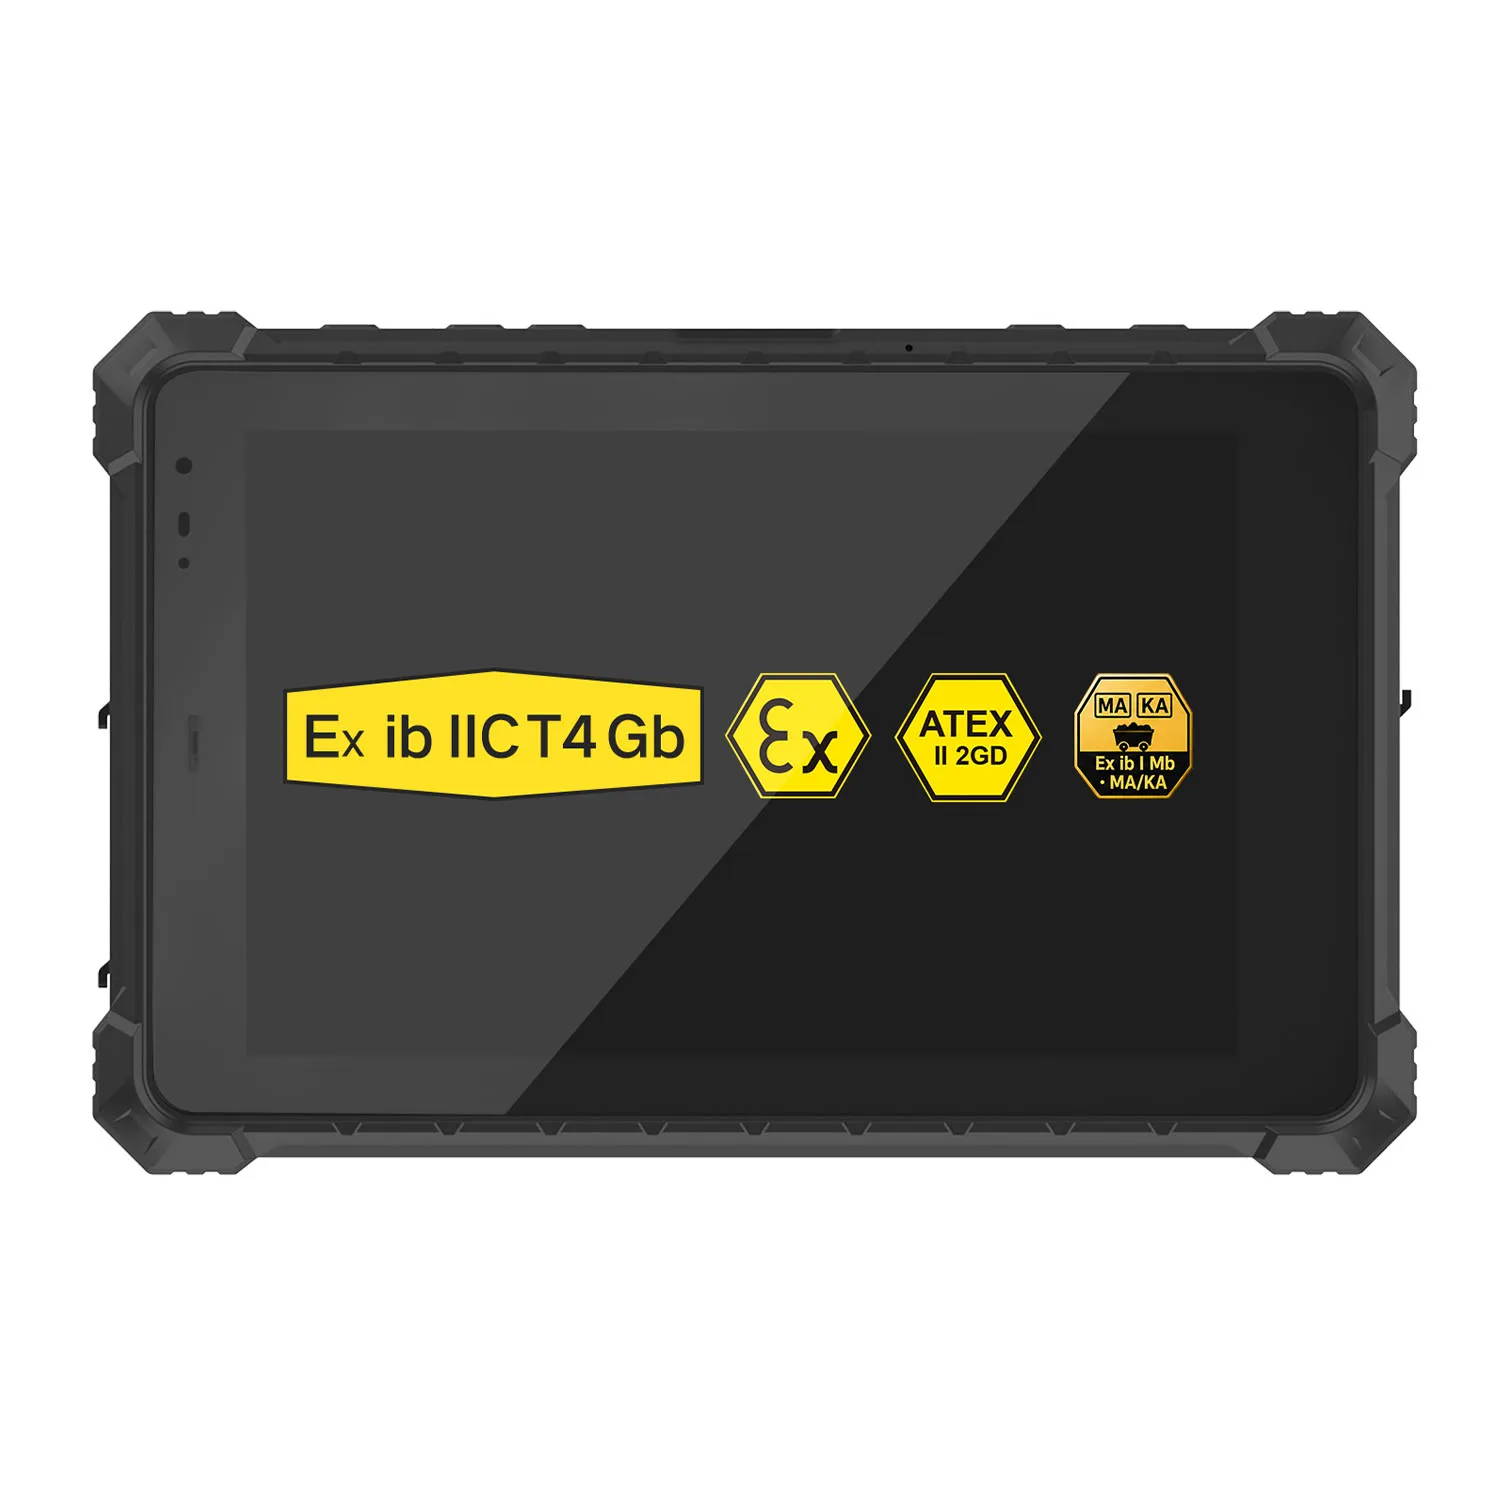
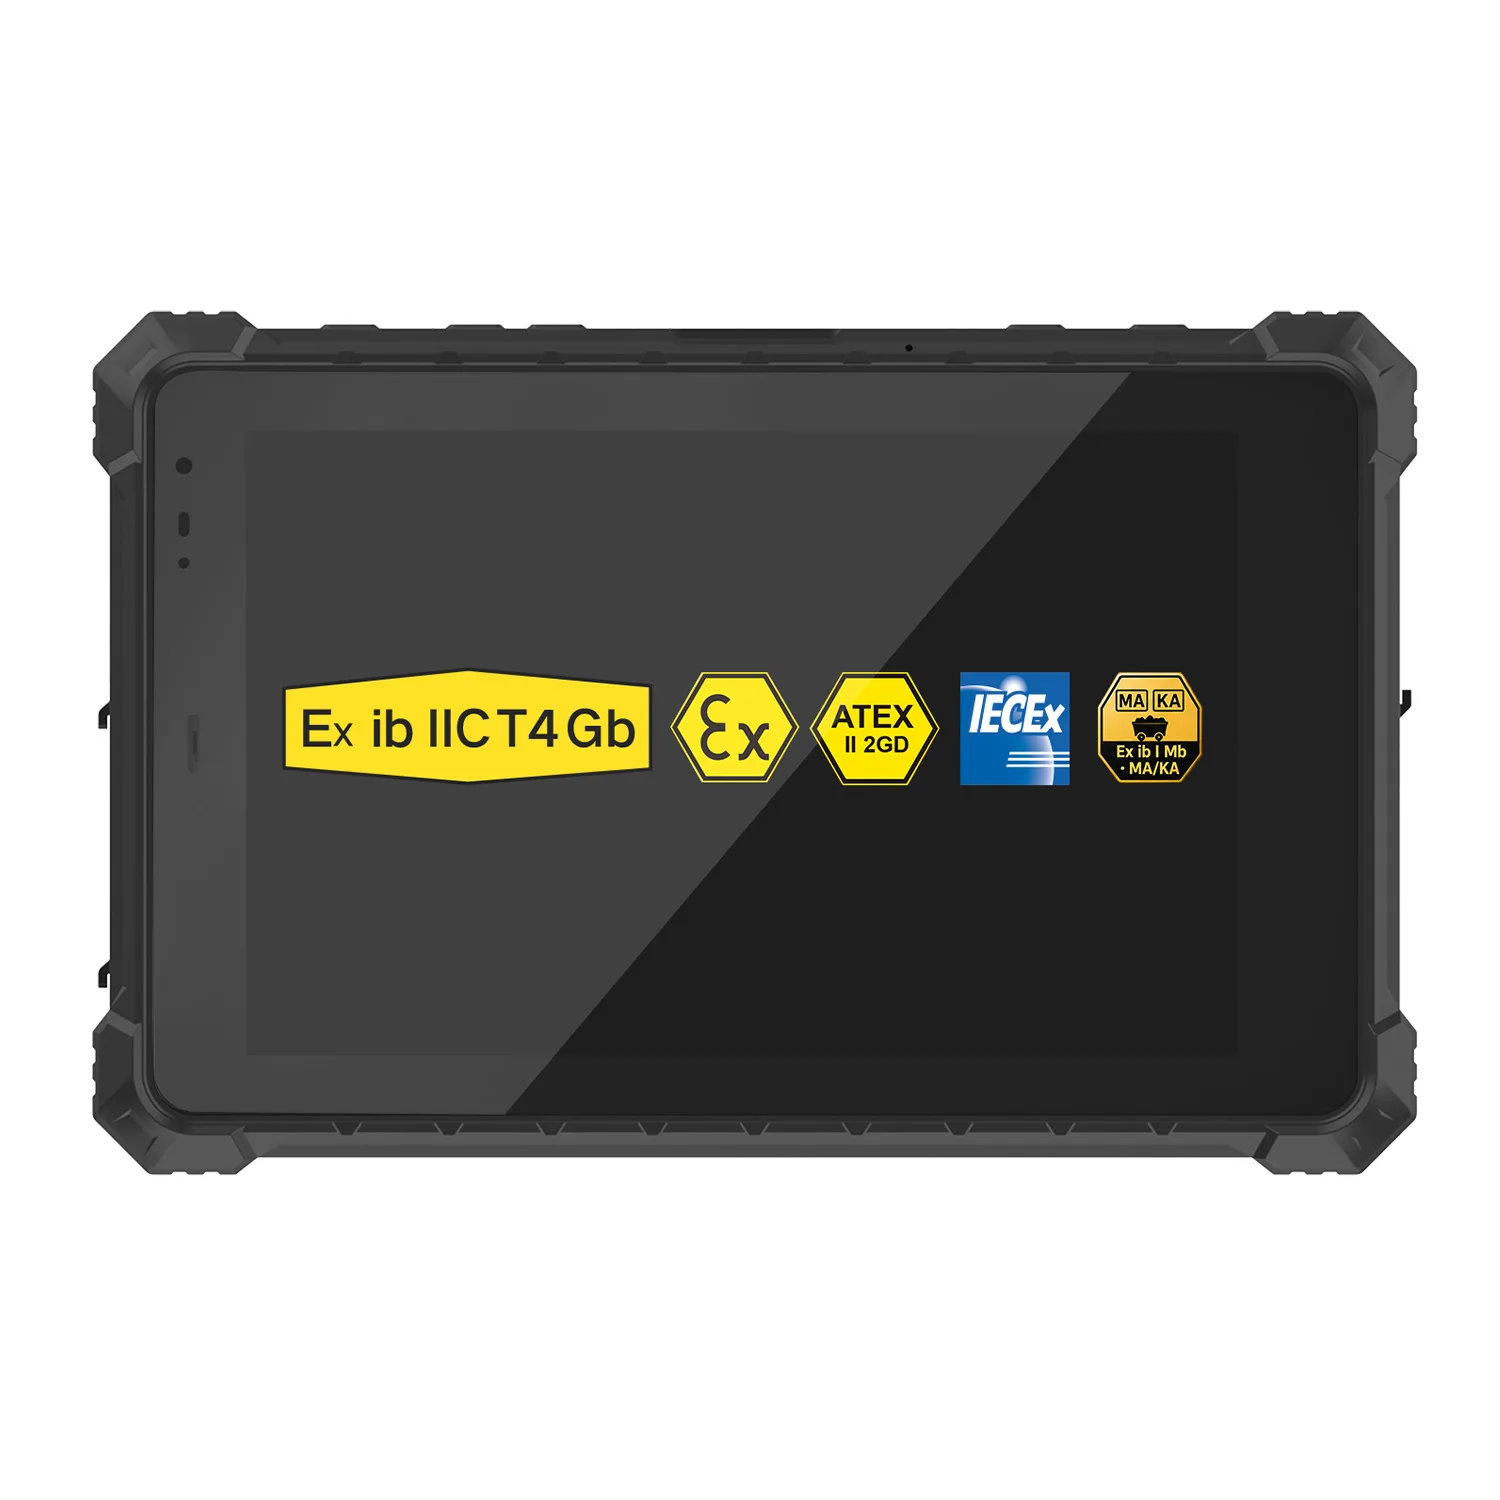
Where an application involves a hazardous or potentially explosive atmosphere, a standard industrial computer should not automatically be treated as suitable.
ATEX, IECEx or other hazardous-location requirements must be evaluated separately, and an appropriately certified explosion-protected product should be selected where required.
Why Manufacturers Choose CENAVA
Platform & lifecycle
Automation platforms stay in our lineup for multi-year production runs, with controlled BOM management — a replacement unit ordered in year three images and mounts like the unit ordered in year one.
Connectivity
RS-232/422/485, CAN, GPIO and dual Gigabit Ethernet are configured per project; the H10F and H10PRO panel PCs cover the common HMI I/O set.
Engineering support
For multi-unit projects, our engineers review CPU platform, I/O, mounting, drivers and BOM before production — the review output is a written configuration sheet attached to the quotation.
Industrial Computers for Pilot Machines and Multi-Site Deployment
A single prototype machine and a large factory rollout have different hardware planning requirements.
During a pilot project, the priority may be confirming software, PLC communication and mechanical integration.
For larger deployments, additional considerations include hardware consistency, operating-system images, driver versions, replacement-unit compatibility and long-term supply planning.
Sort these out at selection time, and year two stops being a surprise.
Talk to CENAVA About Your Automation Project
Start with the machine and the environment — not a generic spec sheet. Send us six things: screen size, operating system, mounting method, PLC and peripheral interfaces, operating temperature, and expected quantity. We will come back with a panel PC or rugged tablet configuration for your HMI, SCADA, MES or data-collection application, plus lead time and pricing.